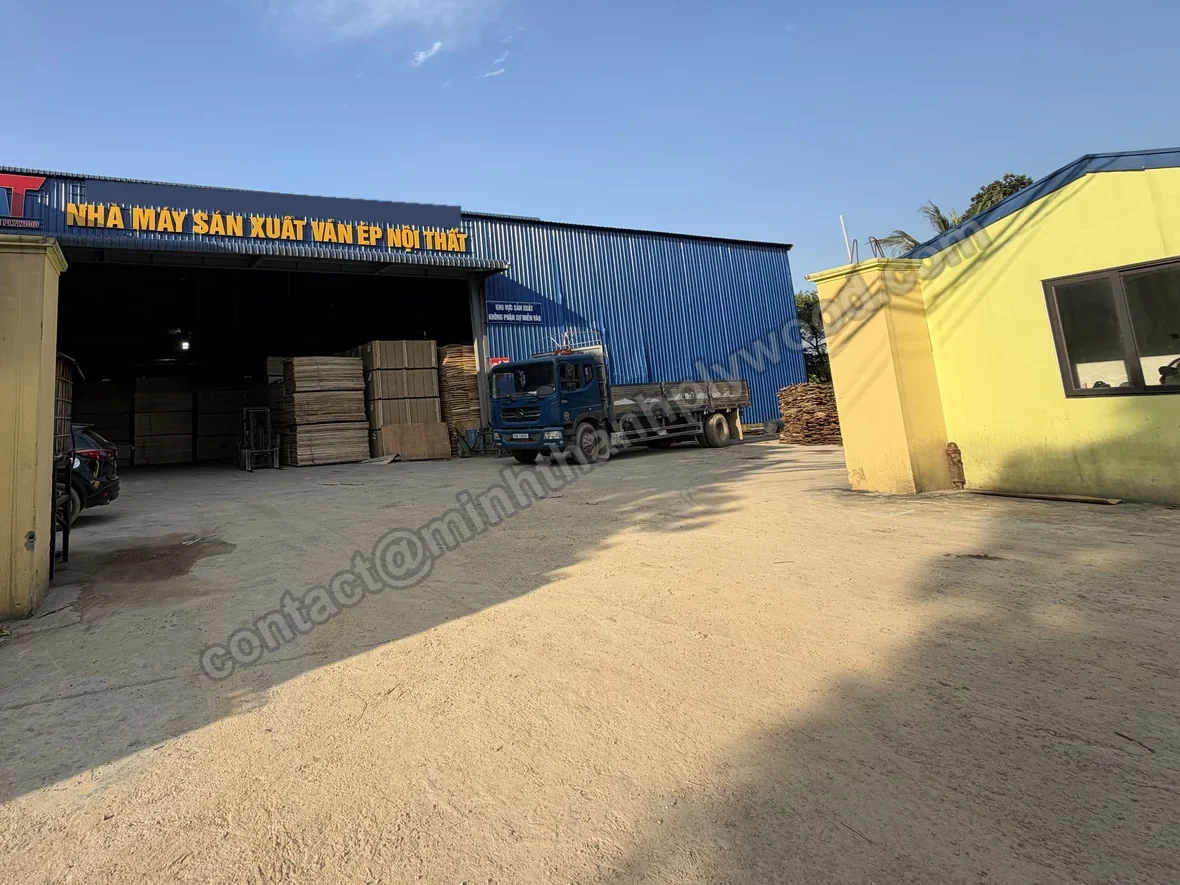
Our factory · Ha Hoa, Phu Tho, Vietnam
Vietnam plywood factory for high-grade furniture panels
In short
Minh Thanh Plywood is a Vietnam plywood factory in Ha Hoa, Phu Tho, built for high-grade furniture and interior plywood, with commercial, packing and film-faced plywood as well. We make 50,000+ m³ a year on local Styrax and Eucalyptus cores, hold CARB P2 / TSCA Title VI and ISO 9001:2015, ship mainly to Europe, and welcome buyer visits and inspections.
Watch the film
Vietnam plywood factory: inside Minh Thanh Plywood, Ha Hoa
The 2:51 film walks through Minh Thanh Plywood from the Ha Hoa location to a sealed container: plantation cores, peeling, stitched lay-up, pressing, sanding down to ±0.2 mm, certificates with their numbers, trade terms and buyer visits. It is cut mostly from real footage of our floor, with captions, so you can judge the factory before you read on.
Who and where (0:00–0:44): a Vietnam plywood factory in Ha Hoa, Phu Tho, built for high-grade furniture and interior plywood, making 50,000+ m³ a year on local plantation Styrax and Eucalyptus cores.
How a panel is made (0:44–1:35): core veneer from local logs, drying and sorting, lay-up stitched both ways, glue to order, hot pressing, calibrated sanding, caliper checks, then packing and container loading.
Proof and terms (1:35–2:51): CARB P2 / TSCA Title VI, ISO 9001:2015 and TCVN 11902:2017, E0 chamber results of 0.014–0.032 ppm, MOQ one 40HC, 15–45 days after deposit, free samples, factory visits and a direct line to Lisa.
Why Ha Hoa, Phu Tho
Why a plywood factory in Ha Hoa gives high grade at a better price.
Ha Hoa gives high-grade plywood at a better price because the core timber grows on the hills around the factory and the workforce is skilled in hand lay-up, stitching and face repair. Logs arrive fresh over a short haul, and finished containers go by road to Hai Phong.
| Advantage | Why it matters | What you get |
|---|---|---|
| Local plantation timber | Styrax and Eucalyptus for cores grow on the hills around the factory, so logs travel a short way and arrive fresh | Lower core cost and steady supply for repeat orders |
| White Styrax core | Styrax is grown in northern Vietnam; it gives a light, pale core of about 500 kg/m³ | Lighter panels, a clean core edge and more m³ per container |
| Face veneer supply | Faces are bought for the look each buyer orders, including imported birch and okoume, and graded in-house | 10+ face veneers on a Vietnamese core |
| Skilled workforce | Plywood making is an established trade in Ha Hoa; hand lay-up, stitching and face repair depend on experienced hands | Furniture-grade construction done routinely |
| Price for the grade | Comparable high-grade mills elsewhere make the same grade at a higher cost | High-grade quality at a better price |
| Road to the port | Containers are loaded at the factory and trucked to Hai Phong | FOB Hai Phong, CFR or CIF to your port |
Many European furniture buyers choose the Styrax core for its light weight and clean face; a Eucalyptus core is denser, at 650–750 kg/m³.
Certified and tested
Certificates you can check before you visit our plywood factory.
We hold CARB P2 / TSCA Title VI (ICTT mill no. 23024), ISO 9001:2015 and TCVN 11902:2017. Six ASTM D6007 chamber tests on 9, 15 and 18 mm E0 panels averaged 0.014–0.032 ppm, against the 0.05 ppm CARB P2 limit. We supply the EUDR compliance dossier (origin records and geolocation files) with orders. FSC and CE are available*. *Supplied directly or through qualified partner mills.
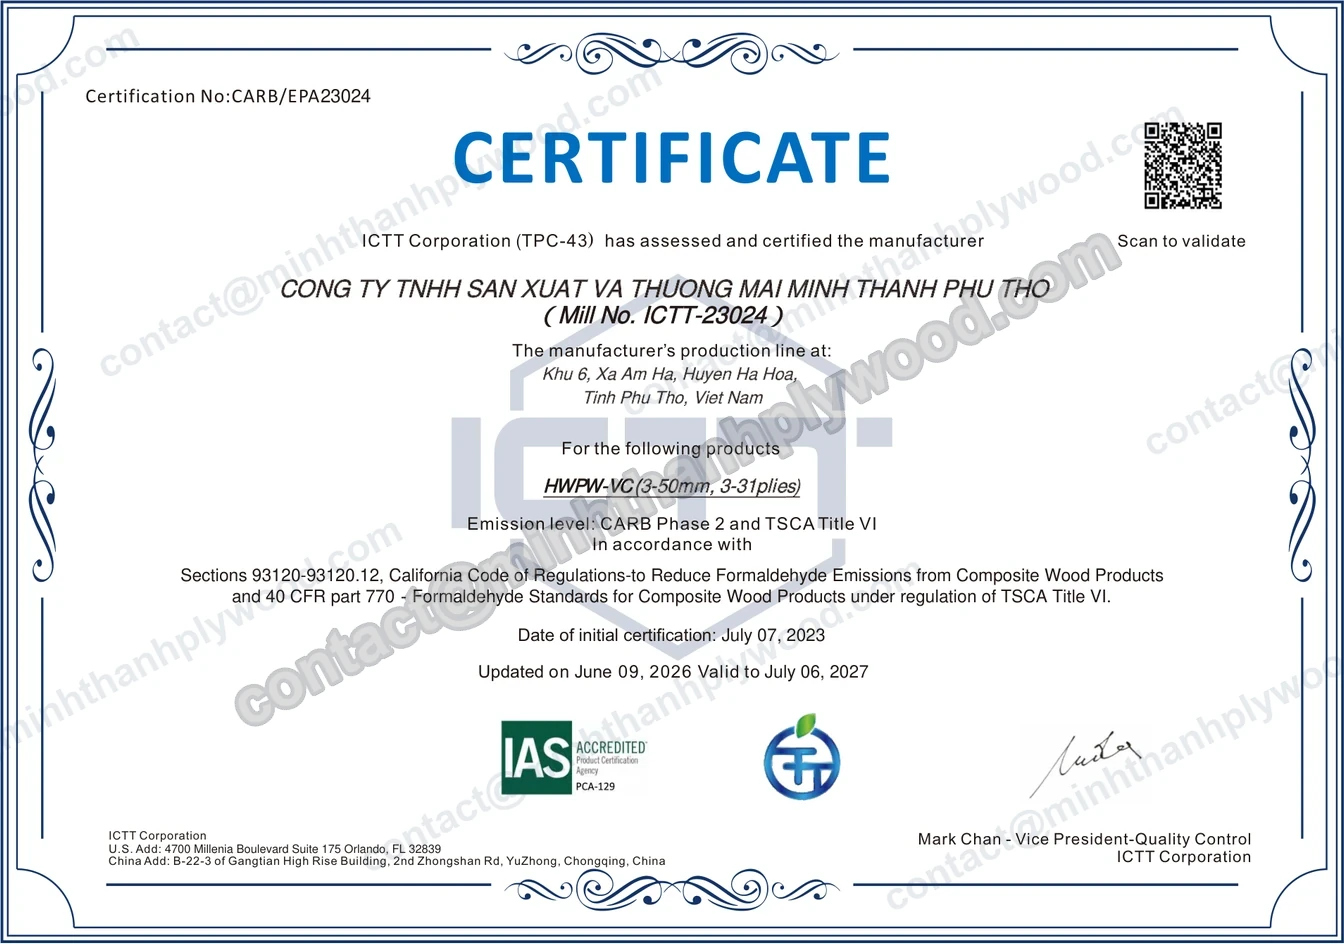 CARB P2 / TSCA Title VIICTT mill no. 23024 · hardwood plywood, 3–50 mm
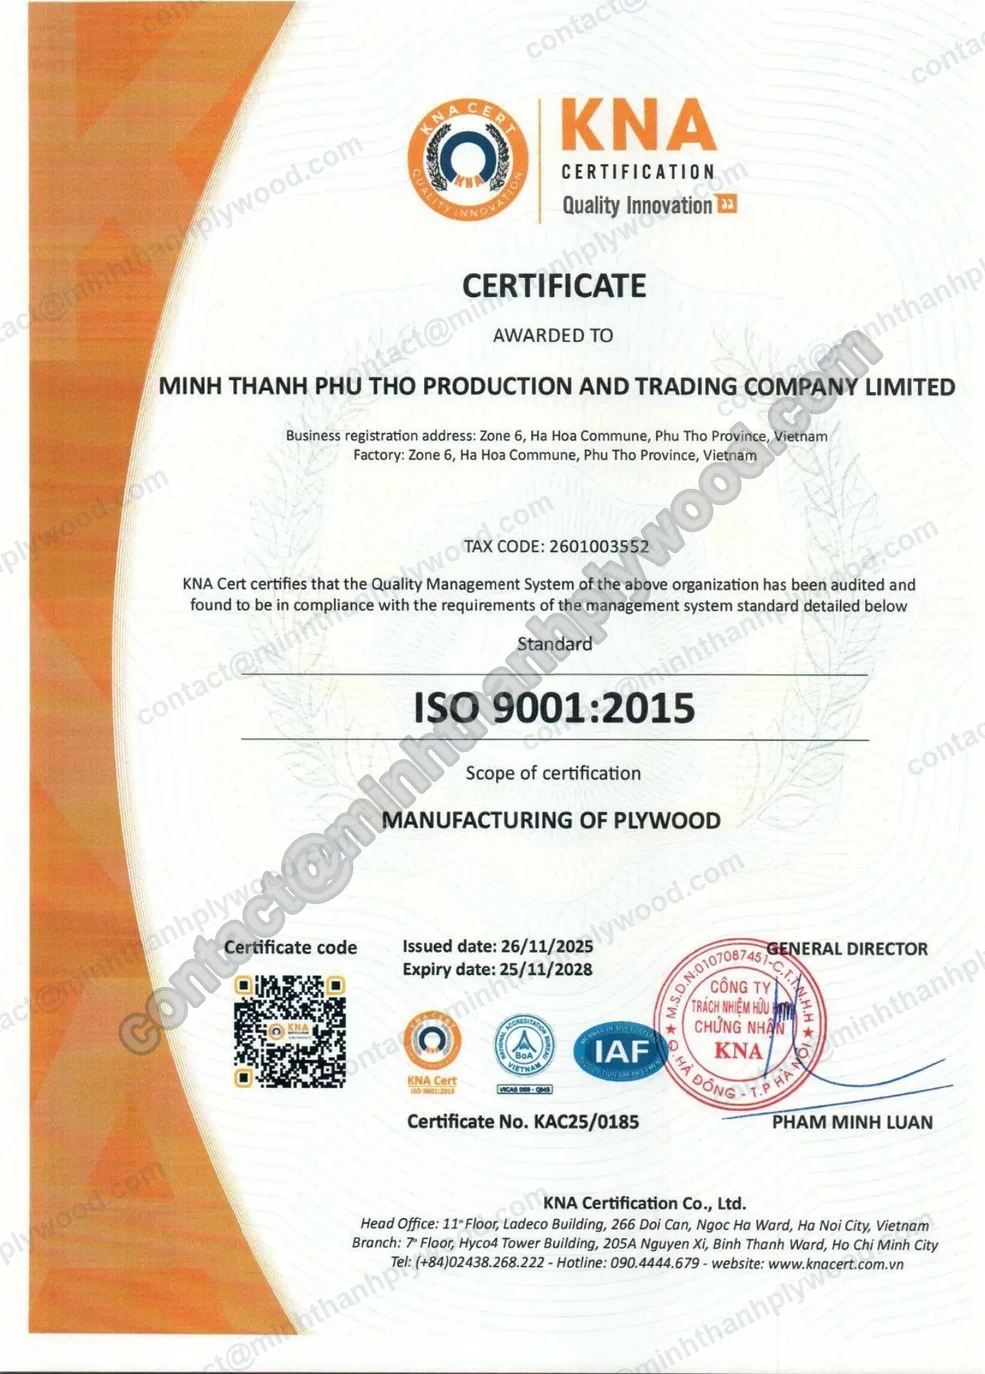 ISO 9001:2015Quality management for plywood manufacturing · KAC25/0185
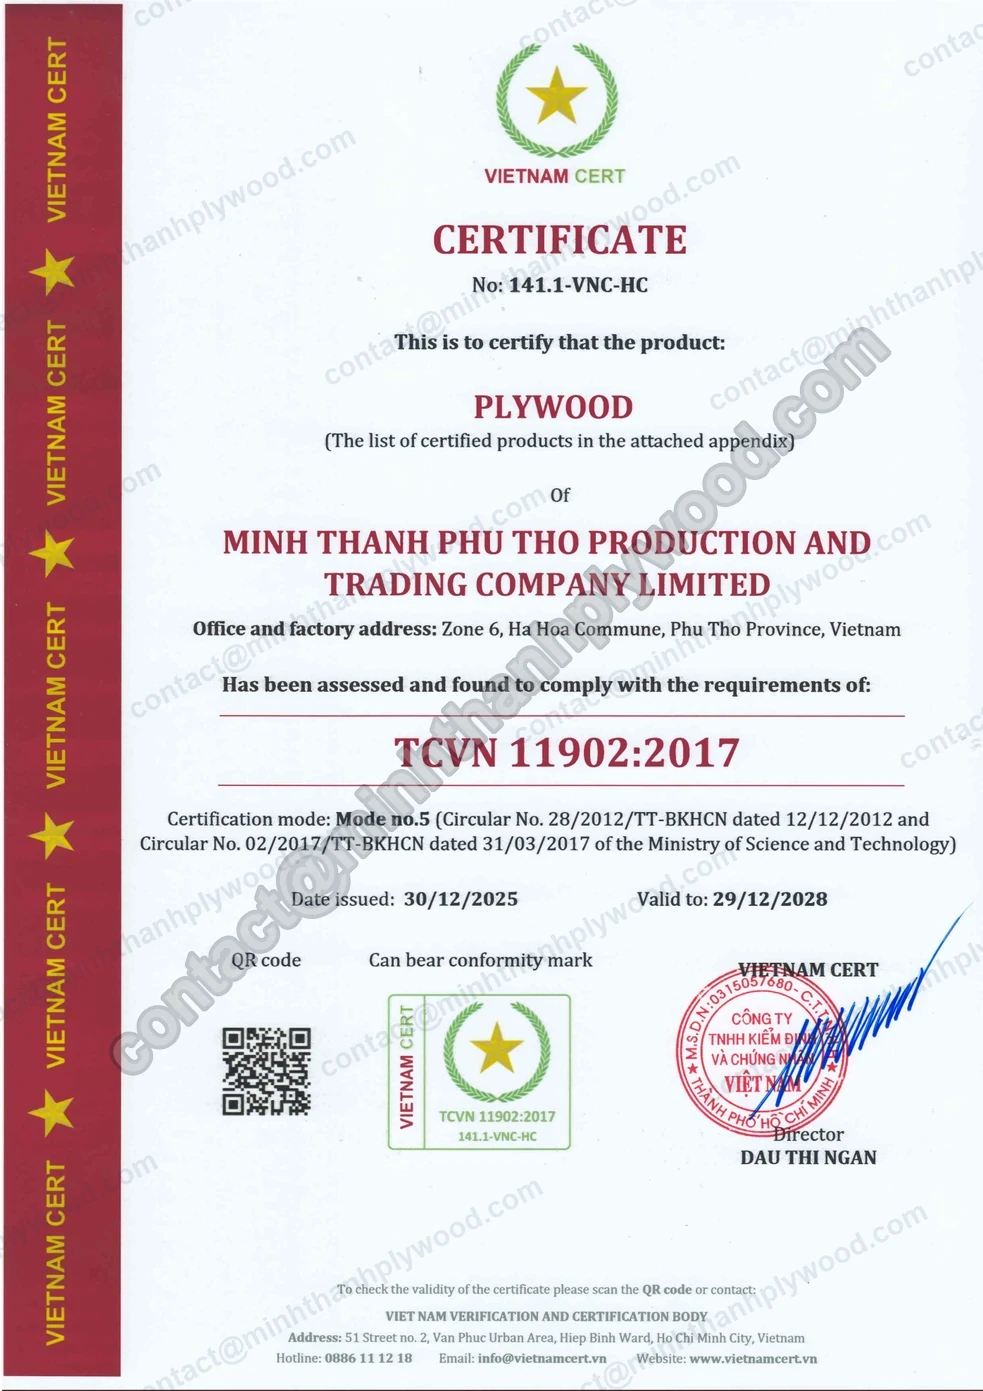 TCVN 11902:2017Certification for veneer-faced plywood
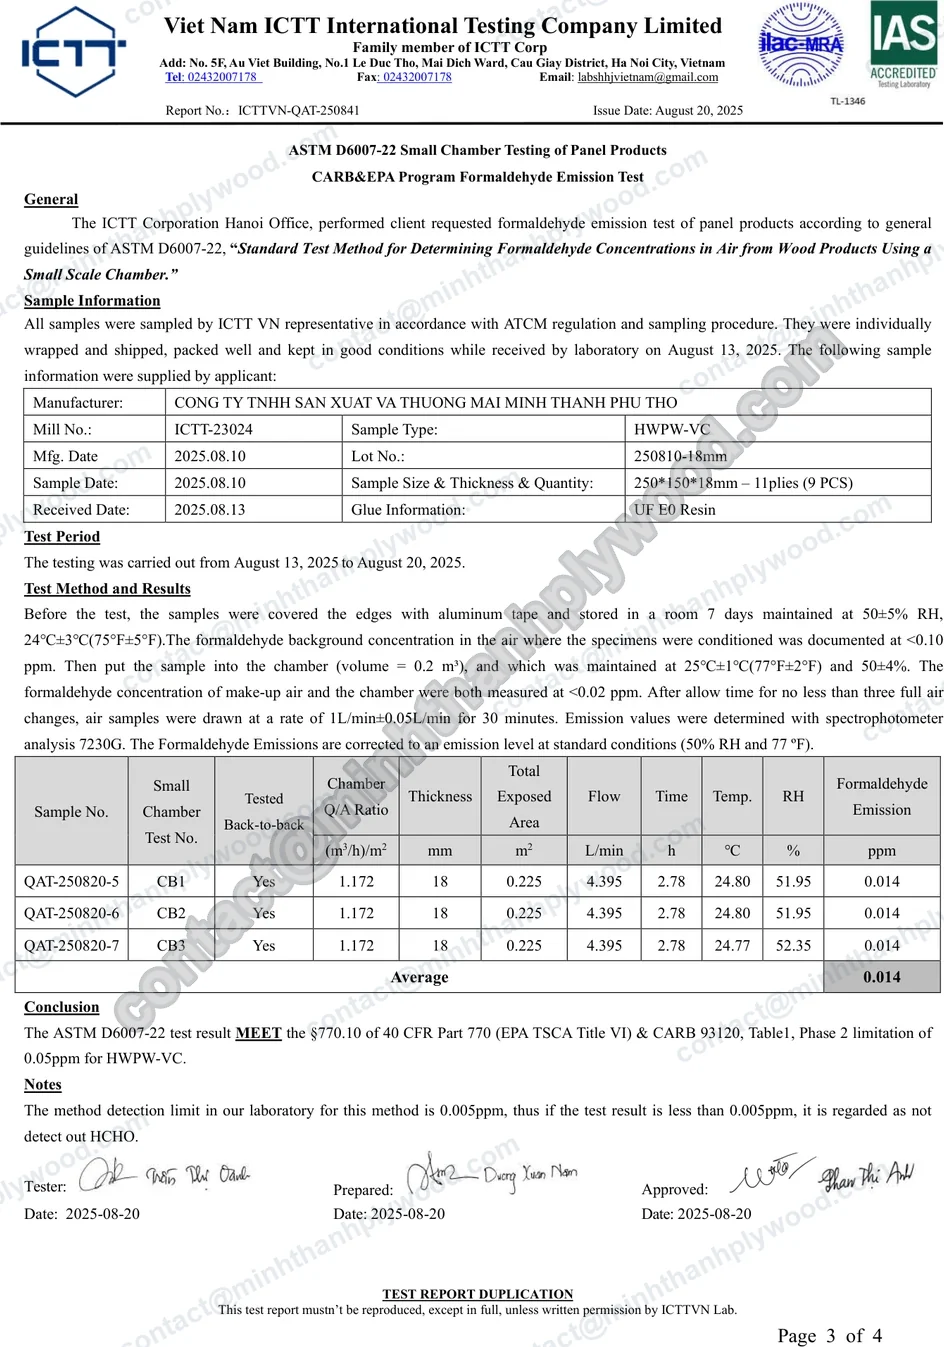 E0 emission testsASTM D6007 chamber · every 3 months · 0.014–0.032 ppm
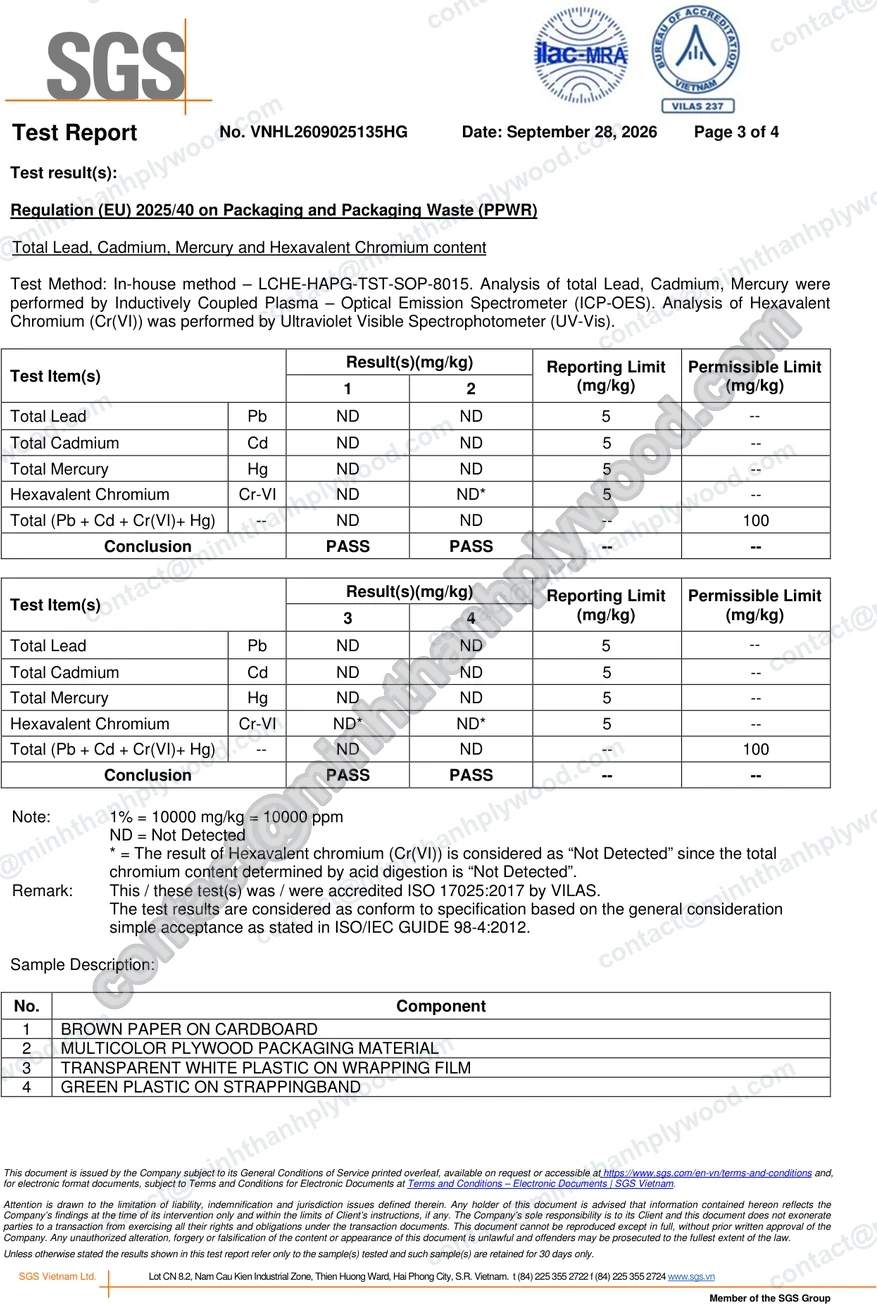 PPWR packaging testSGS, September 2026 · heavy metals not detected
Who we are
Minh Thanh at a glance: plywood company, Vietnam, factory-direct.
Minh Thanh Plywood is a manufacturer, not a trading desk: our own teams in Ha Hoa peel, lay up, press, sand, check and pack the panels in your container, and you deal directly with the people who make them.
In shortMinh Thanh Plywood is a Vietnamese plywood manufacturer in Ha Hoa, Phu Tho province, northern Vietnam, built for top-grade furniture and interior plywood with Europe as its main market. We also produce commercial, packing and film-faced plywood. Capacity is 50,000+ m³ a year, and the team brings over 20 years of plywood-making experience to every order.
| Item | Minh Thanh Plywood |
|---|---|
| Business type | Plywood manufacturer and exporter, factory-direct |
| Location | Ha Hoa, Phu Tho, northern Vietnam |
| Built for | Top-grade furniture and interior plywood; Europe is the main market |
| Production | 50,000+ m³ a year |
| Experience | Over 20 years of plywood making, focused on furniture-grade panels |
| Also produced | Commercial, packing and film-faced plywood; anti-slip, exterior (CDX-type) and LVL |
| Cores | White Styrax or Eucalyptus from local plantations |
| Faces | 10+ veneers; most produced EV, Poplar, Birch, Okoume, Pine |
| Thickness and sizes | 3–40 mm; 1220 × 2440 and 1250 × 2500 mm, plus custom sizes |
| Certificates held | CARB P2 / TSCA Title VI, ISO 9001:2015, TCVN 11902:2017 |
| Markets | Europe (strongest), the Americas, Asia, Africa |
| Minimum order | One 40HC container, mixed loads by agreement |
| Export contact | Lisa, international sales, in English by email, WhatsApp or video call |
| Email and WhatsApp | [email protected] · +84 988 586 601 |
Office hours: Monday–Friday, 08:00–17:00 Vietnam time (UTC+7). Replies within hours.
Product range
Three product groups from one plywood factory.
Our plant makes three product groups: furniture and interior plywood as the main line, commercial and packing plywood, and construction and exterior panels. Each group has its own core grade, glue and tolerance, so one Vietnam plywood factory can fill a mixed container with the right build for each use.
| Group | Products | Core and construction | Glue | Thickness tolerance | Typical uses |
|---|---|---|---|---|---|
| Furniture & interior | Birch, Poplar, EV, Okoume, Pine, Eucalyptus-faced, Gurjan, Bintangor; thin 3–6 mm; cut-to-size; Sapele on request | A-grade Styrax or Eucalyptus core, stitched both ways, sanded and polished, UV-ready | UF glue at E0 emission as standard; E1 emission, MR or WBP glue to order | ±0.2–0.3 mm | Cabinets, furniture parts, drawer boxes, shelving, interior fit-out |
| Commercial & packing | Commercial plywood, packing plywood | AB-grade core, laid or jointed; light sanding or unsanded | To order | Commercial ±0.5 mm; packing ±0.5–1.0 mm | Crates, pallets, packaging, general building and joinery |
| Construction & exterior | Film-faced, anti-slip, exterior / CDX-type, LVL | Acacia or Eucalyptus core; film 120–135 g/m², premium from 135 | Melamine-fortified or phenolic (WBP) | ±0.5 mm | Concrete formwork, flooring, stair treads, sheathing, beams and frames |
All groups: 1220 × 2440 and 1250 × 2500 mm, custom sizes such as 1220 × 2500 and 1220 × 2280 mm; length and width ±2 mm.
Production process
How our plywood factory makes a panel, in nine steps.
Plywood is made by peeling logs into thin veneer, drying and grading it, gluing the sheets in cross-banded layers, pressing them cold and then hot, and sanding the panel to thickness. In our Vietnam plywood factory every panel follows nine steps from plantation log to sealed container, and each step has a check a failed panel cannot pass.
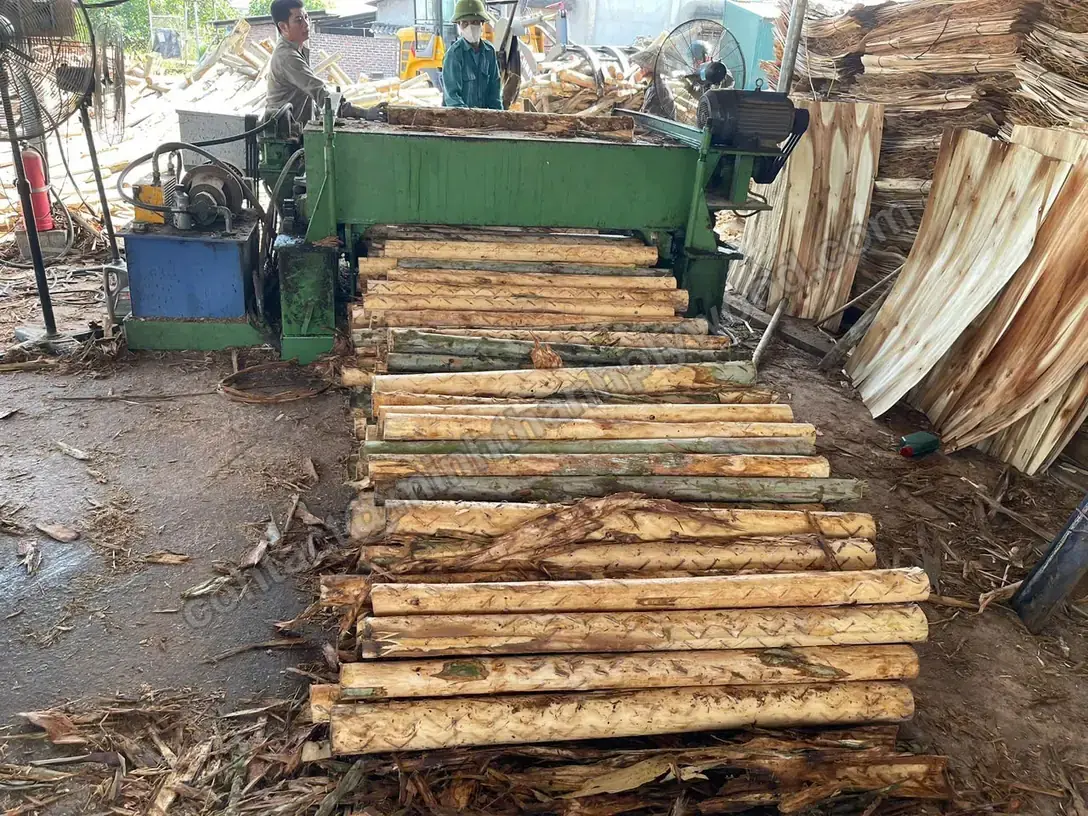
Eucalyptus logs waiting at a rotary peeling line. 01Plantation logs to core veneer
Eucalyptus and Styrax logs come from plantations around Ha Hoa. Rotary lathes peel them into continuous core veneer, which is clipped to sheet size.
- Logs from plantations around Ha Hoa
- Veneer peeled fresh for an even, clean sheet
- Core veneer thickness set by the panel build
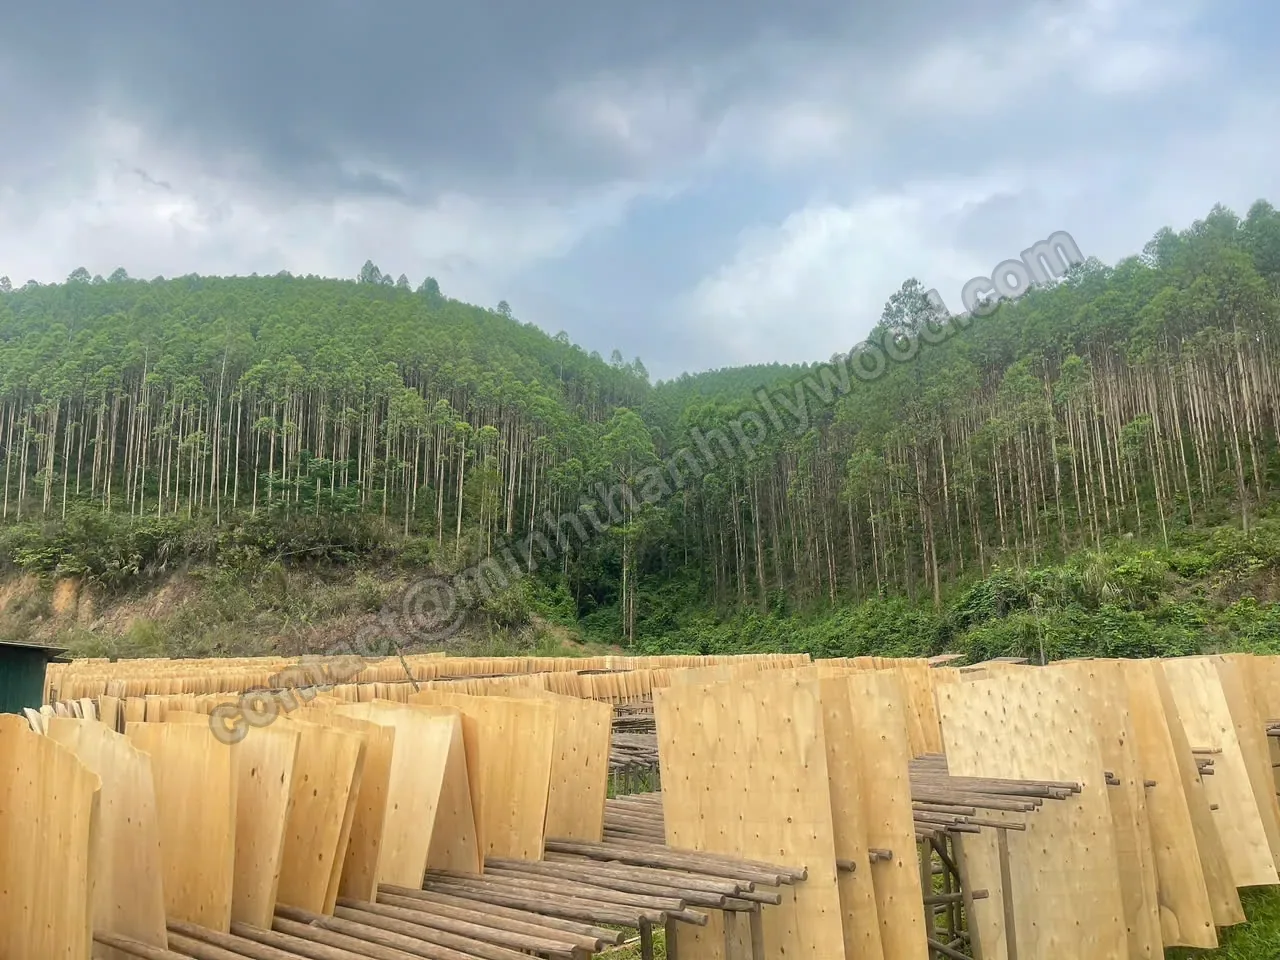
Core veneer drying in front of eucalyptus plantation hills. 02Sun drying
Core veneer is dried on racks in the open air, then stacked under cover. Dry veneer is the first defence against warping and blisters later.
- Veneer dried before sorting and lay-up
- Damp or warped sheets go back to the racks
- Dry veneer stored under roof
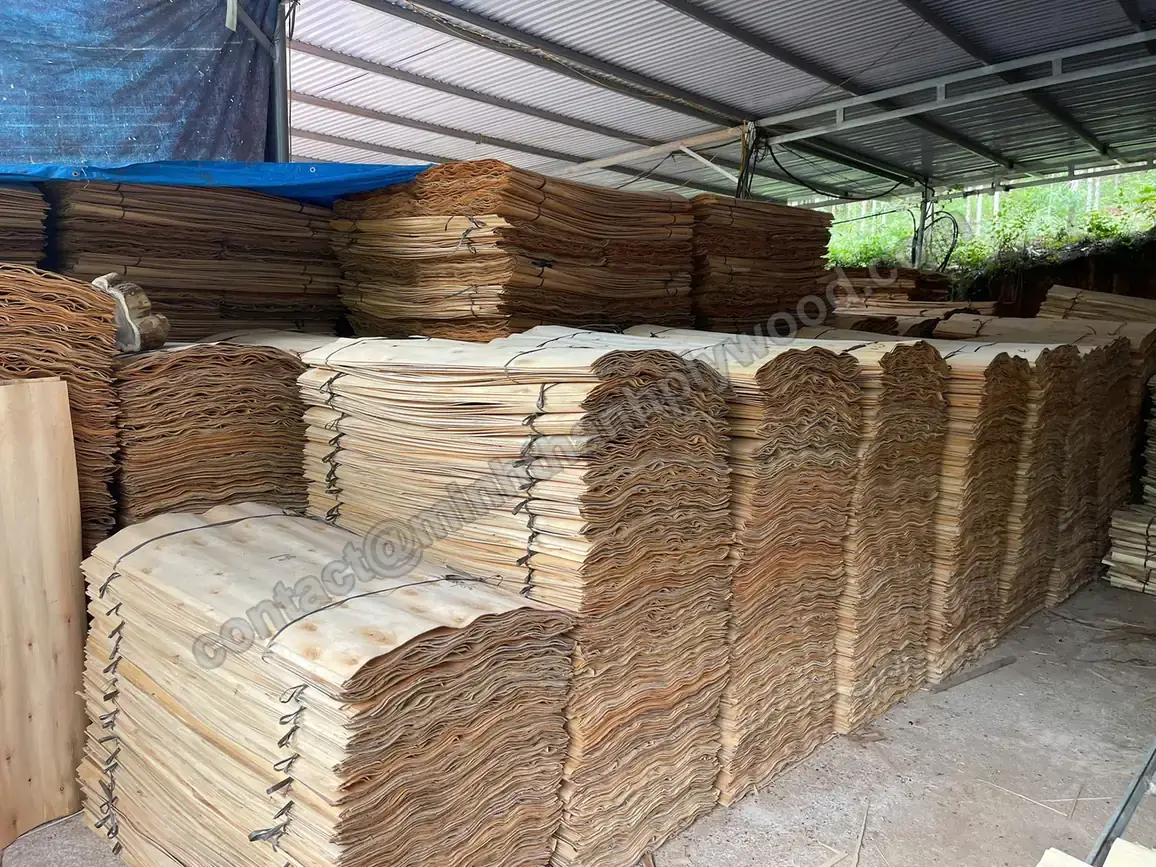
Sorted core veneer bundles under cover. 03Veneer sorting and grading
Dried veneer is sorted by grade. Splits, holes and soft sheets are taken out, and face veneer is matched to the sample you approved.
- Core sorted into A and AB grades by line
- Face veneer matched to your approved sample
- Birch faces graded D+, D or E, quoted as pairs such as D+/D
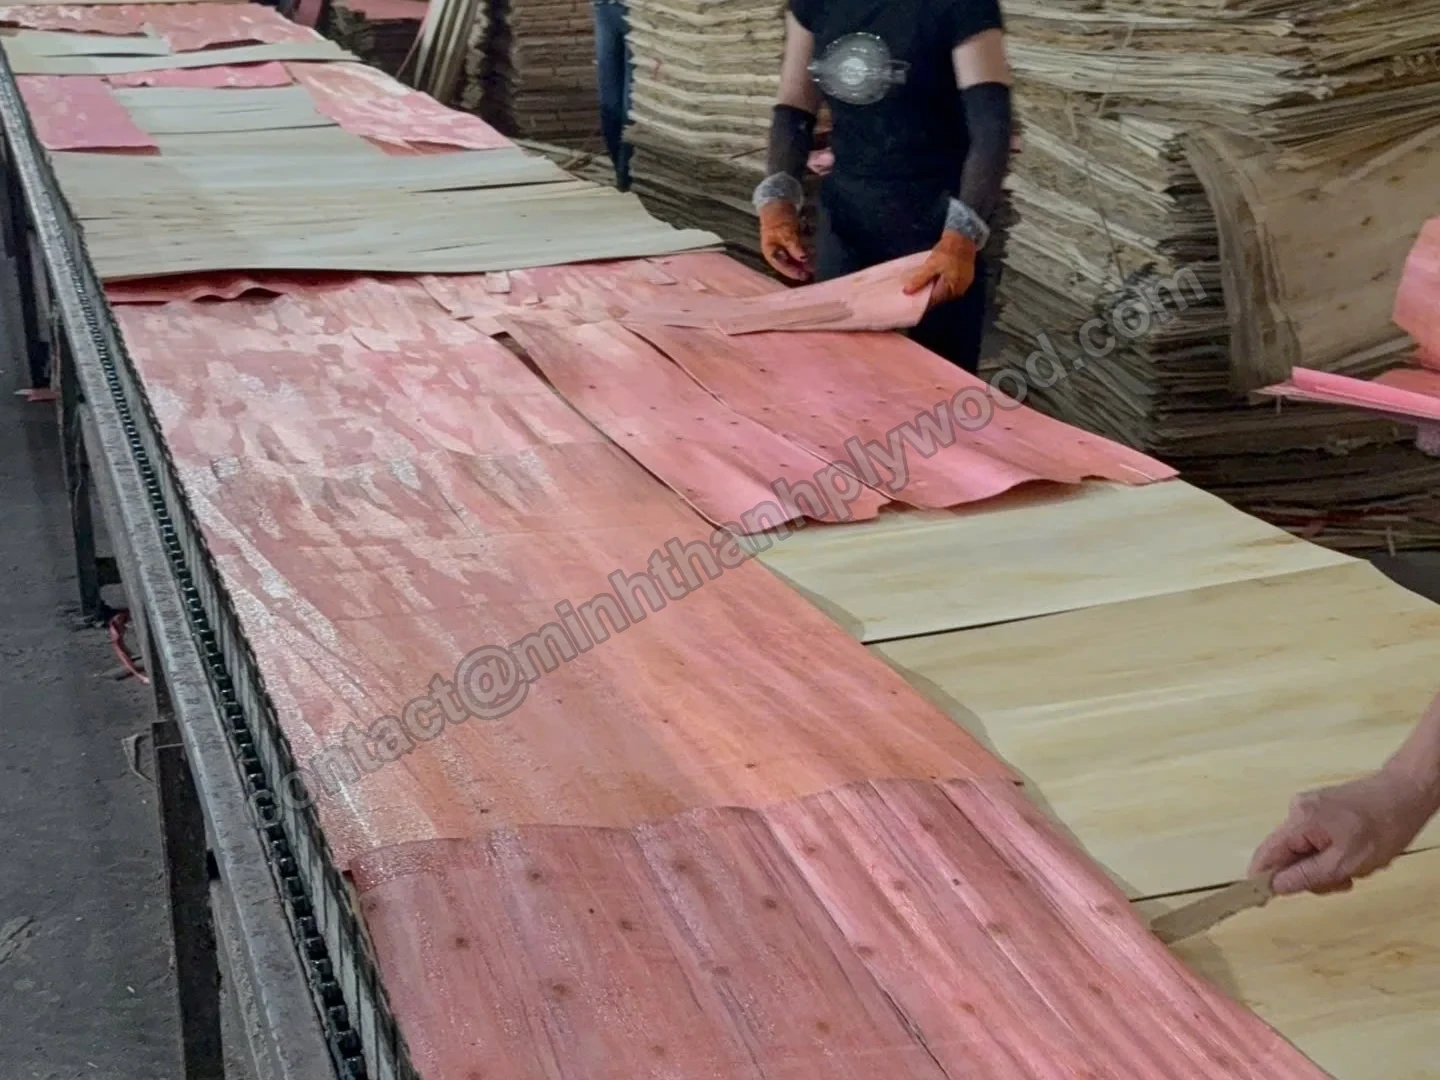
Glued core veneer laid up by hand on the line. 04Glue spreading and lay-up
Glue is mixed to your order and spread on the core veneer. Cores are laid by hand in cross-banded layers, and the outer core layers are stitched horizontally and vertically.
- UF glue at E0 emission as standard; E1 emission, MR or WBP glue to order
- Outer 2–4 core layers stitched both ways; all layers on request
- 18 mm: 11–13 plies, most often 11; 3–6 mm always 5-ply
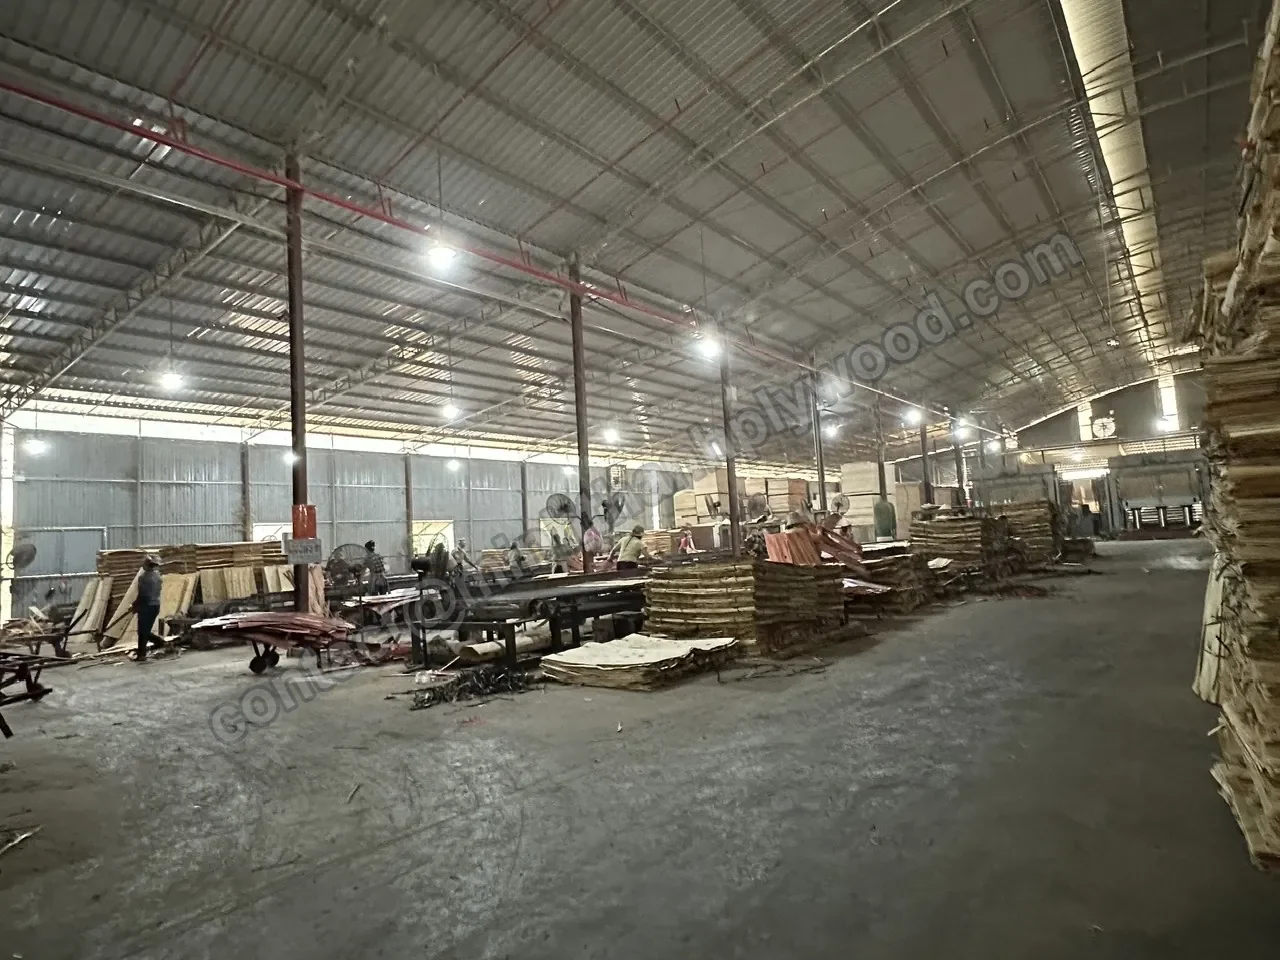
Production hall: lay-up area in front, hot presses at the far end. 05Cold and hot pressing, twice for furniture panels
Laid-up panels are cold pre-pressed, then cured in multi-opening hot presses. Furniture-grade panels are pressed twice: the core board is pressed and calibrated, then face and back are pressed on for a flat, even face. Press temperature follows the glue: 110–120 °C for MR-type glue and 130–145 °C for WBP.
- Press temperature set by the glue system
- Core board calibrated before faces go on
- Bond checked on sample pieces by boil test
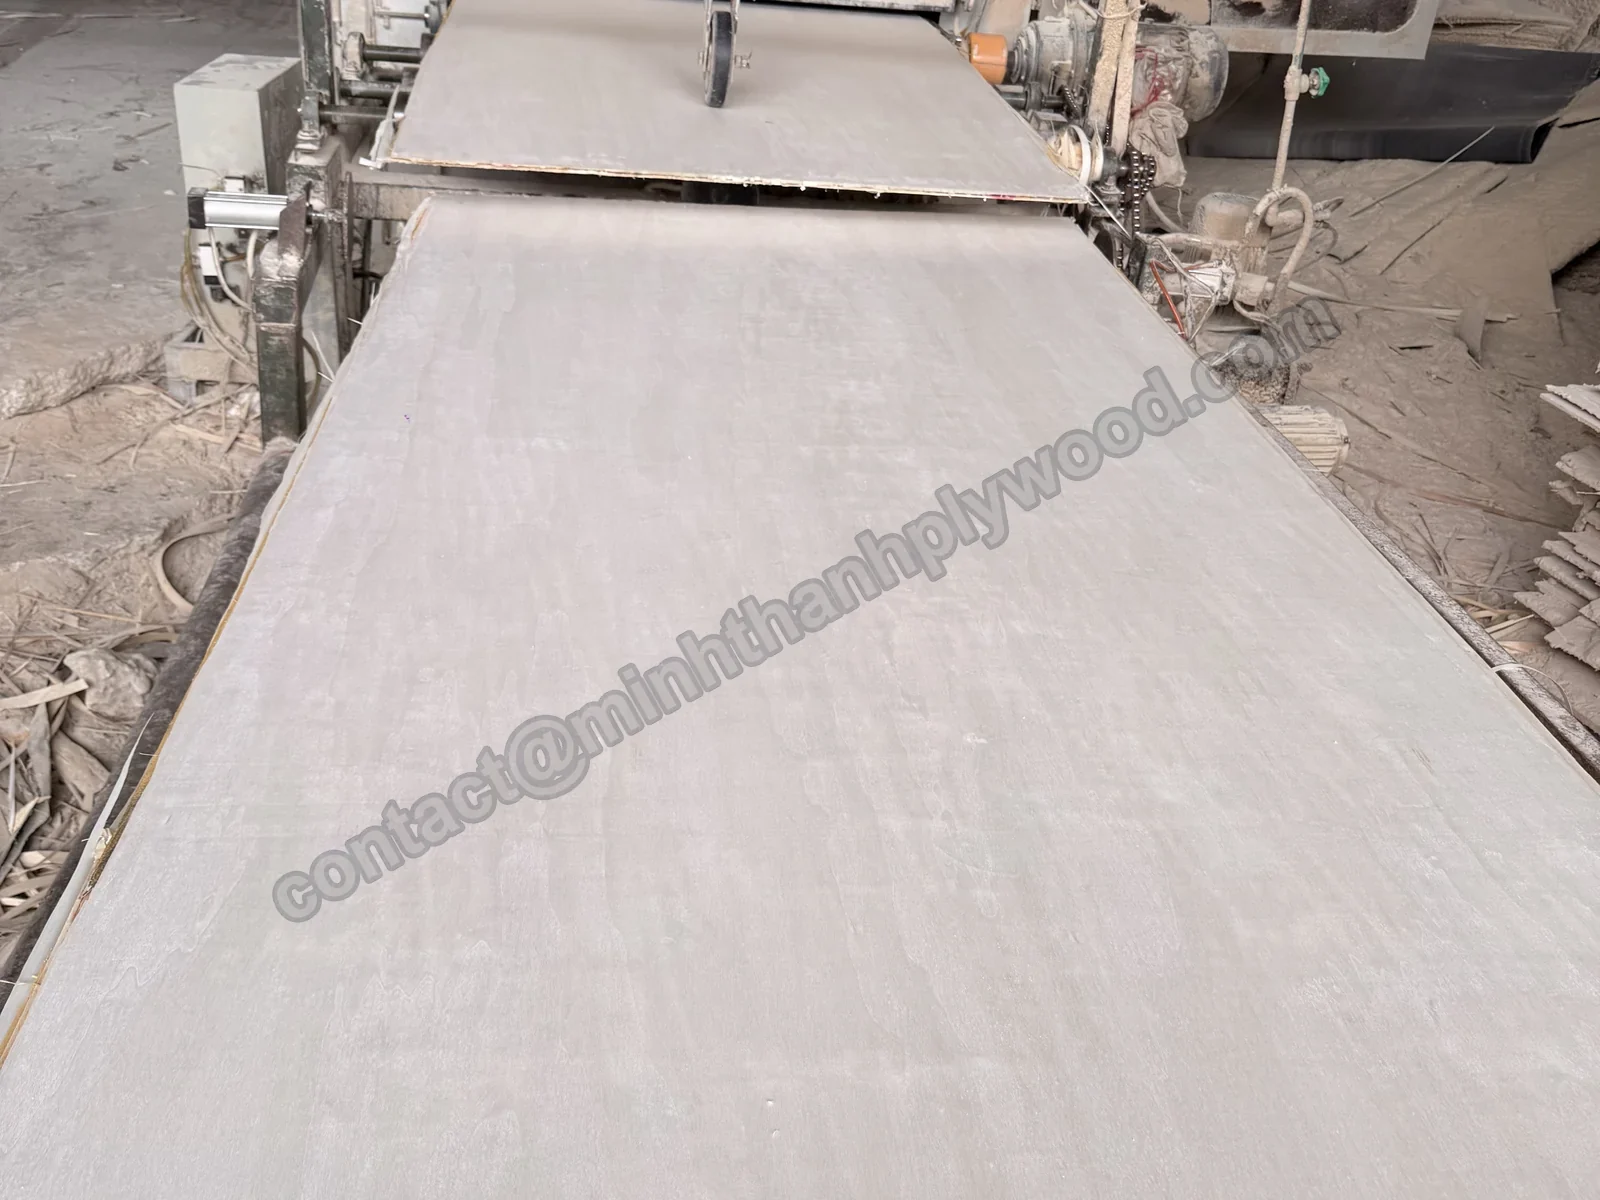
Panels on a calibrating sander. 06Calibrated sanding
Pressed panels are trimmed to size, repaired where needed, then run through calibrating and finishing sanders. Furniture panels reach their final thickness and a smooth, UV-ready face here.
- Thickness calibrated before finish sanding
- Both faces sanded and polished
- Faces left UV-ready for your own coating
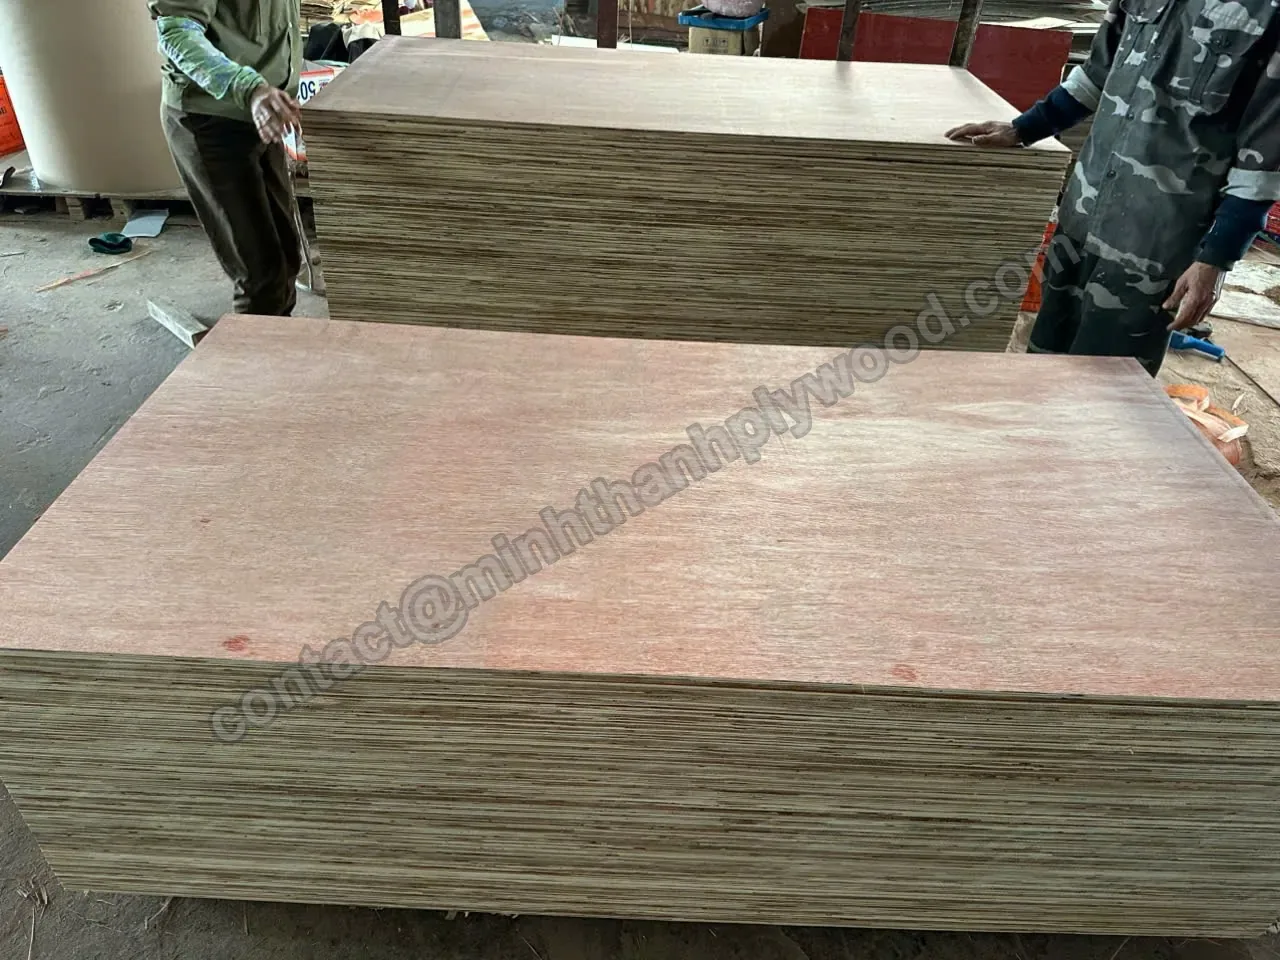
Finished panels stacked for grading. 07Face grading and thickness check
Finished panels are graded face by face against your sample and measured with a digital caliper on every pack. Panels outside the agreed tolerance do not go into your order.
- Furniture panels down to ±0.2 mm
- Length and width ±2 mm, corners checked for square
- Edges free of open gaps and delamination
- Readings sent with the shipment photos
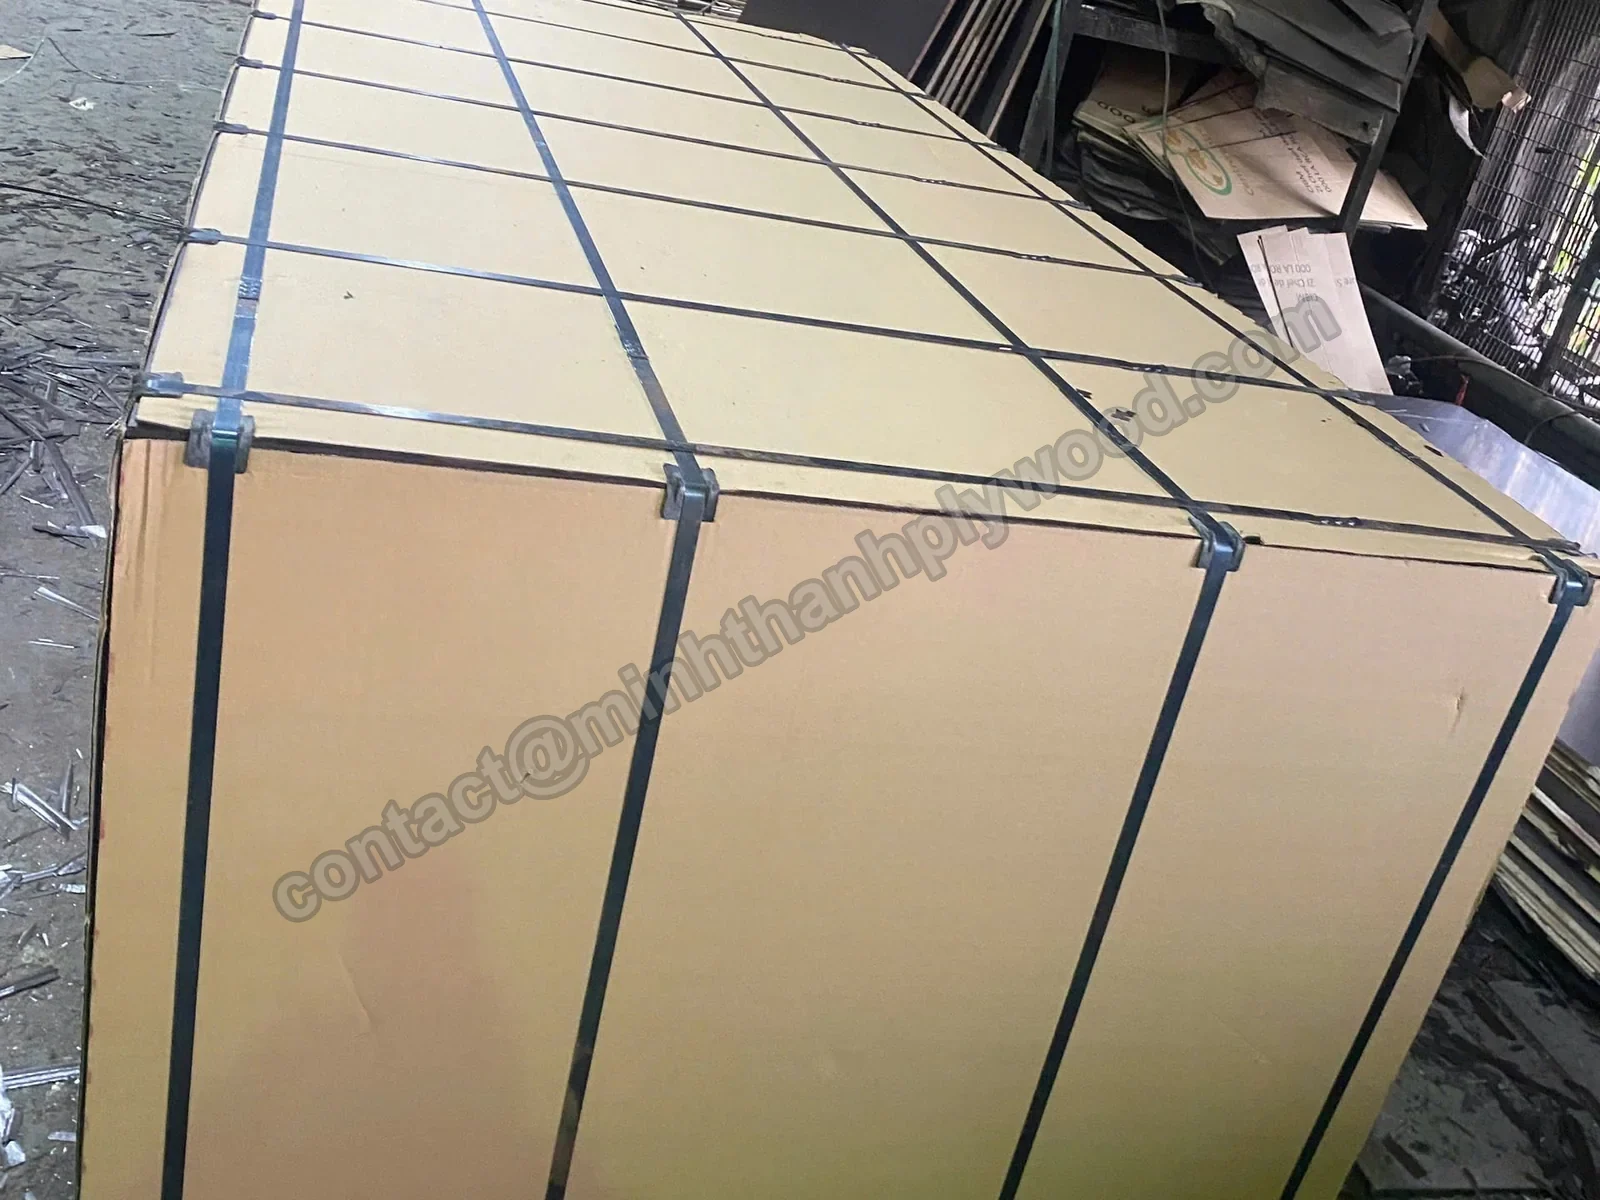
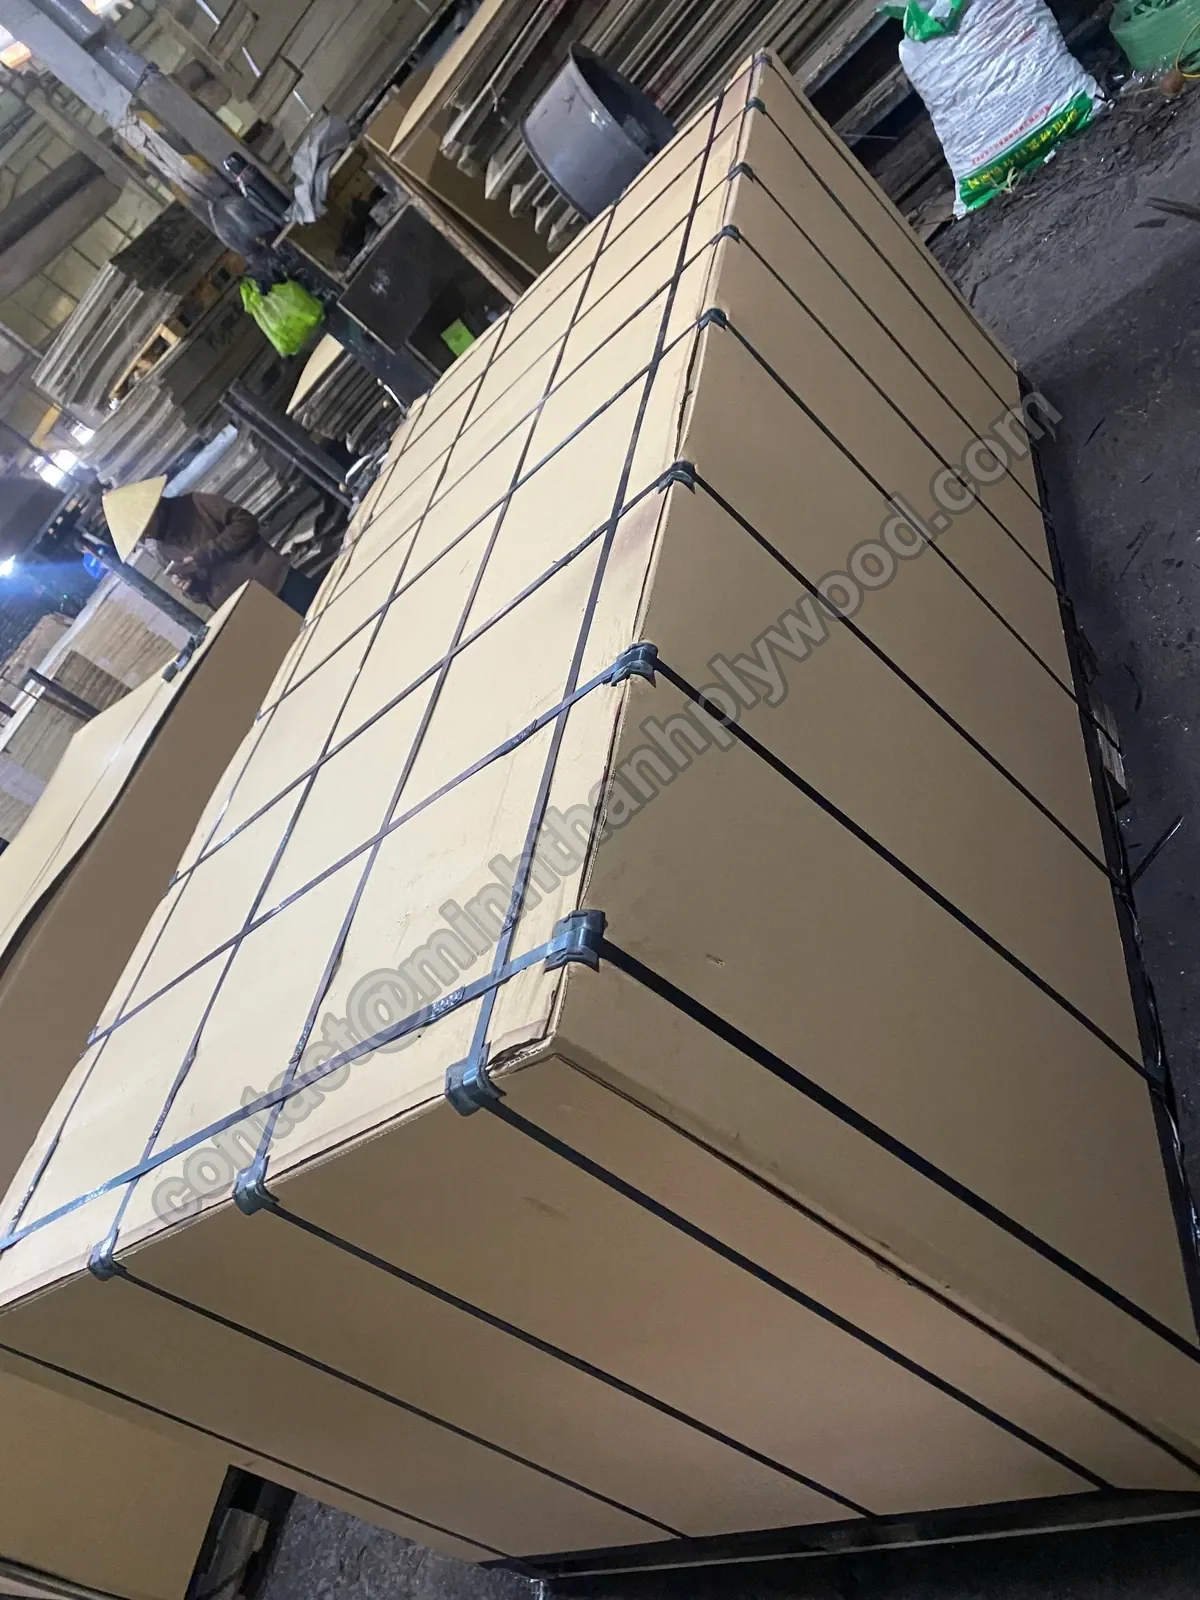
Export pack: cardboard cover and steel straps. 08Export packing
Packs are counted against the packing list, covered with cardboard, fitted with corner guards and strapped with steel bands on export pallets. Your own labels, pack marks and edge printing are applied here.
- Pack height about 1,000 mm
- Cardboard, corner guards, steel straps
- Customer labels and edge printing on request
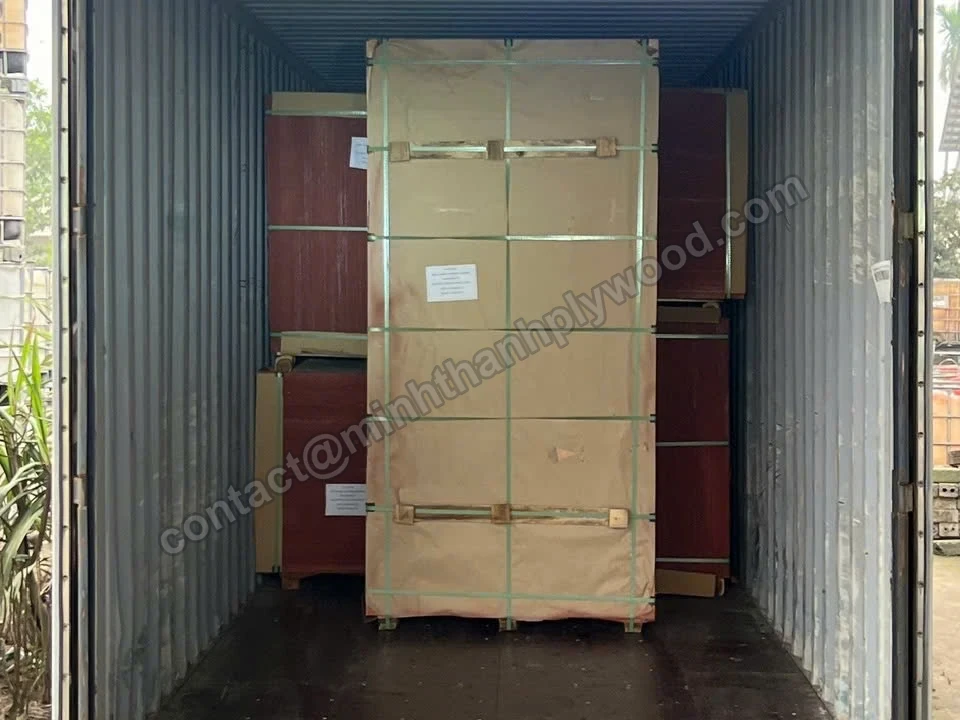
Packs loaded into a 40HC container. 09Container loading
Packs are loaded into 40HC containers at the factory by forklift, secured and trucked to Hai Phong. Loading is photographed and filmed, and the record goes to you before the container is sealed.
- Up to 18 packs per 40HC with Styrax core
- About 53–54 m³ per 40HC with Styrax core
- Photos and video before sealing
Real factory videos
Watch the plywood factory floor at work.
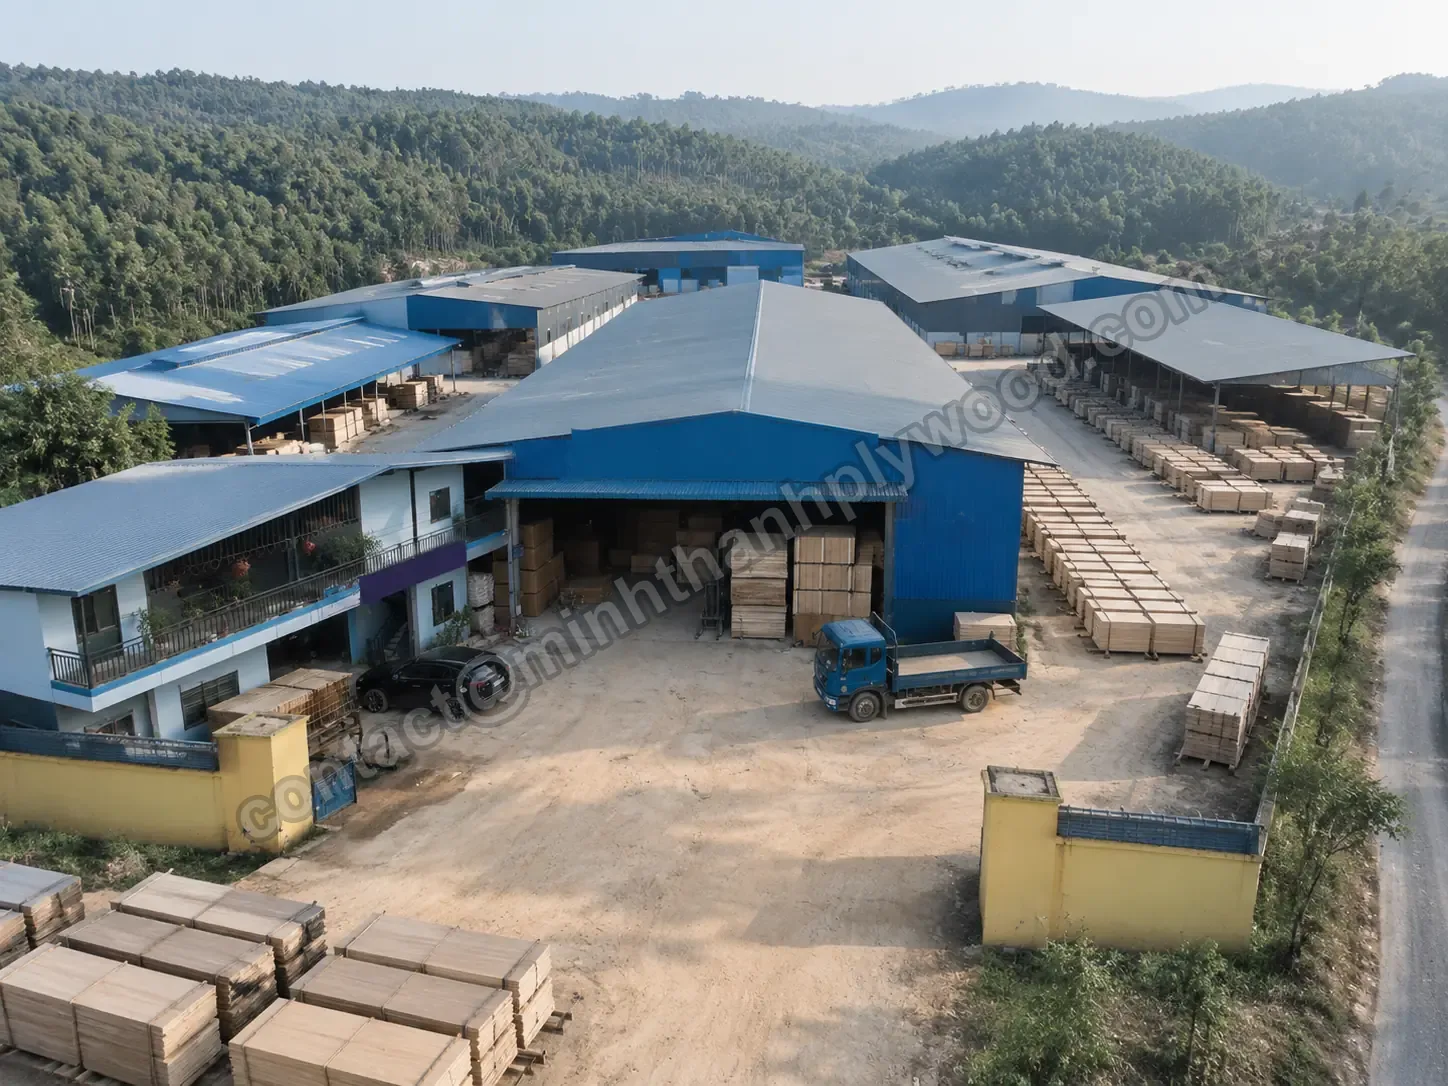
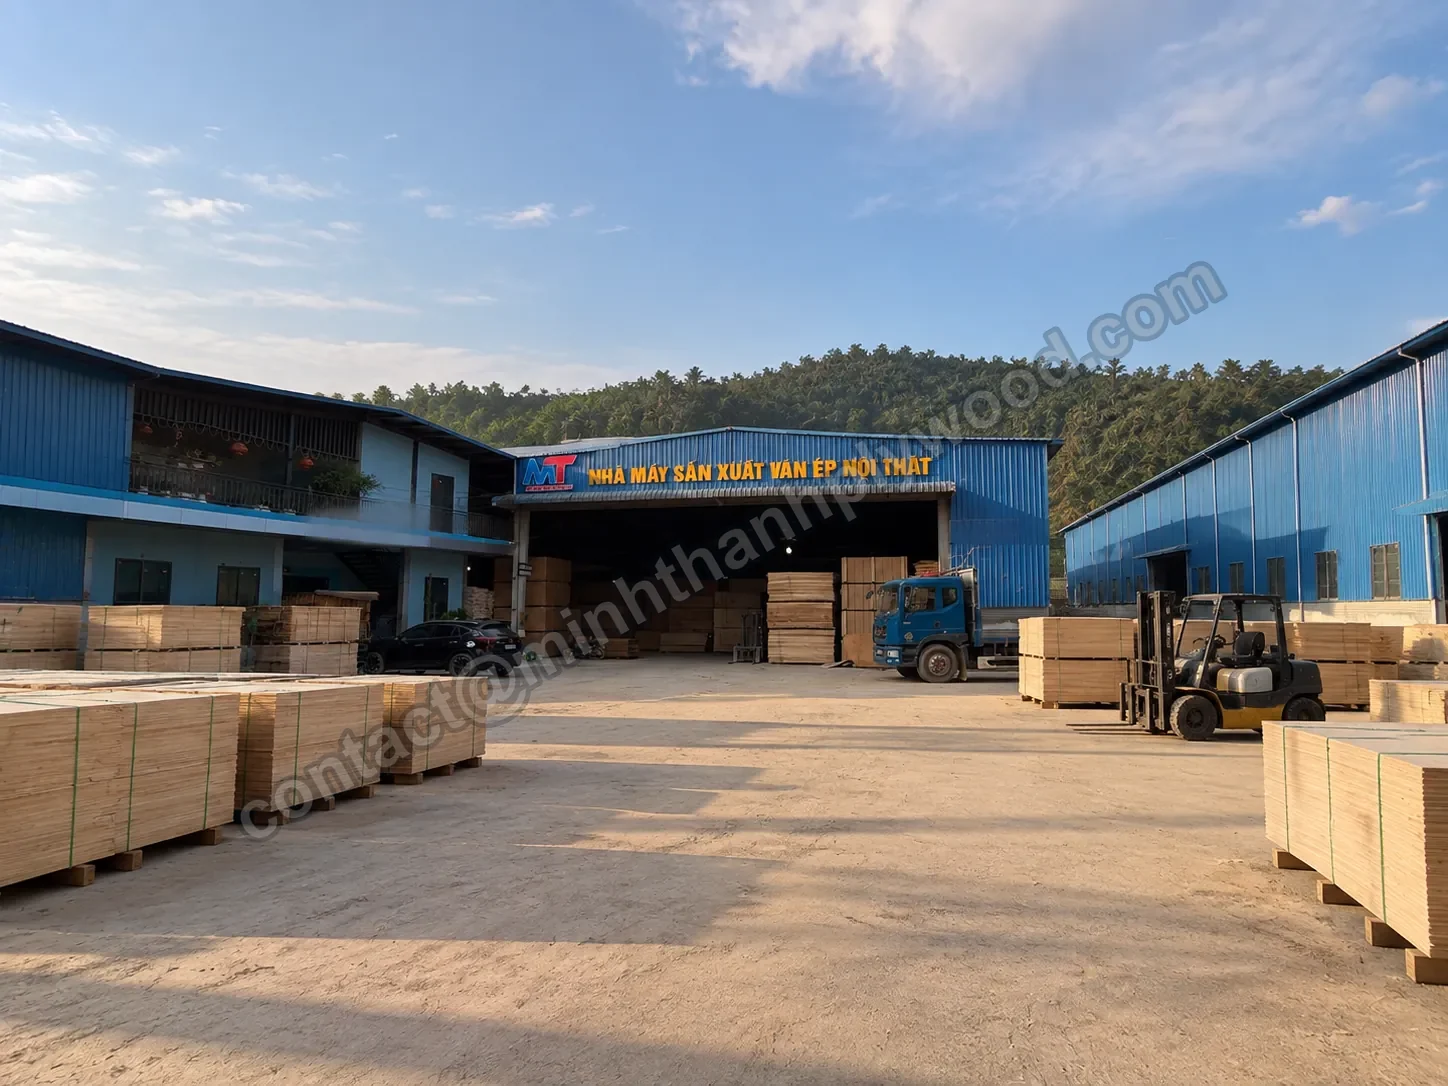
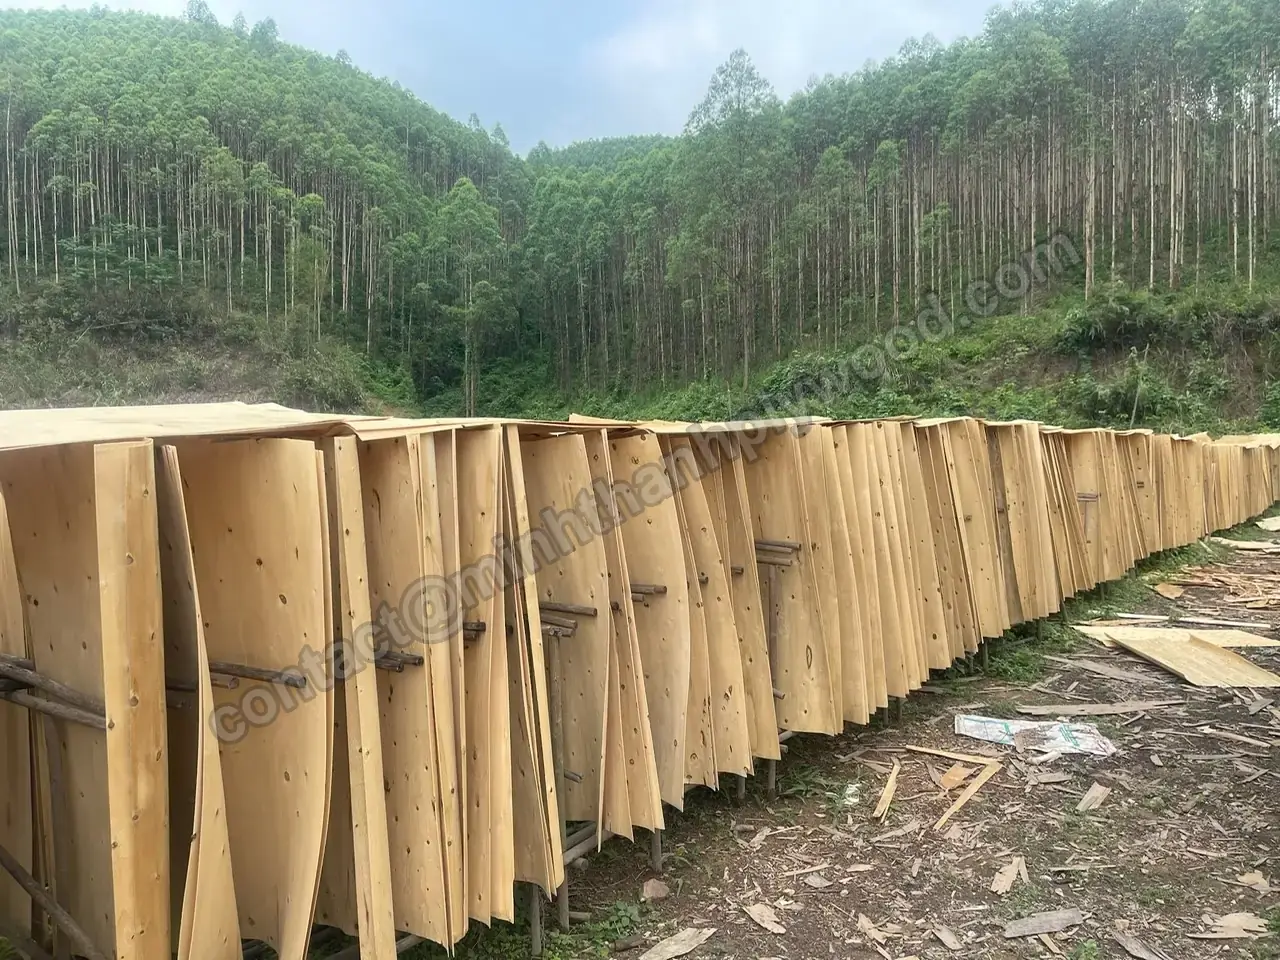
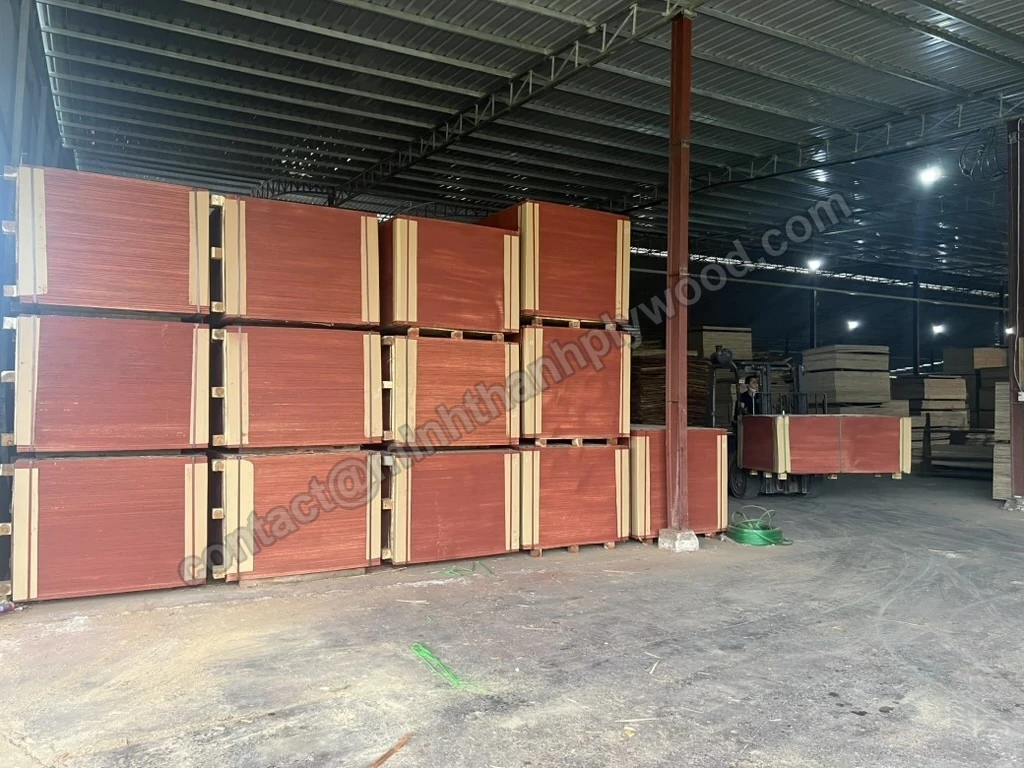
These clips are filmed on our own production floor in Ha Hoa: veneer warehouse, lay-up hall, glue spreader, core composer, hot press and panel turner. They play muted when you scroll to them, and the photos below show the site, drying racks and warehouse.
Trade terms
Trade terms for orders from our plywood factory.
Orders start at one 40HC container, production takes 15–45 days after deposit, and payment is 30% deposit with 70% against the scanned B/L, FOB Hai Phong, CFR or CIF. An order moves from your specification to a quotation, a free sample, the deposit, production, your inspection and loading.
| Order steps | Specification → quotation → free sample → deposit → production → inspection → loading record → B/L |
|---|---|
| Minimum order | One 40HC container |
| Mixed loads | Usually 1–2 products per container; 3–6 by agreement |
| Production time | 15–45 days after deposit; transit is separate |
| Payment | 30% deposit, 70% against the scanned B/L |
| Payment methods | T/T or irrevocable L/C at sight |
| Incoterms | FOB Hai Phong, CFR or CIF |
| Samples | Free samples |
| Shipment record | Photos and video of every container before sealing |
| Inspection | Your inspector or a third-party agency welcome before loading |
| Documents | Invoice, packing list, B/L, C/O (EUR.1 for the EU), phytosanitary and fumigation where required |
| Reply time | Within hours, Monday–Friday 08:00–17:00 (UTC+7) |
Quotations are priced on face, core, glue, thickness, size and quantity: send your specification and Lisa replies within hours.
Official sources: CARB composite wood products (Phase 2) · US EPA TSCA Title VI formaldehyde standards · ISO 9001 quality management · ASTM D6007 chamber method · EU Deforestation Regulation (EU) 2023/1115 · EU Packaging Regulation (EU) 2025/40 · FSC certification · ICC Incoterms® 2020
Verify before you buy
How to tell a real plywood factory from a trading desk.
A real plywood factory can show five things on request: a certificate with its own mill number, dated test reports with a method, its production floor live, edge photos of your own order, and compliance files before the deposit. Minh Thanh shows all five.
Certificates name the mill. A CARB P2 / TSCA Title VI certificate carries the mill number of the plant that makes the panels; ours is ICTT mill no. 23024. ISO 9001:2015 KAC25/0185 covers plywood manufacturing, not only trading.
Test reports come with a method and a date. Our E0 panels are tested in a third-party chamber every 3 months: six ASTM D6007 tests from April 2025 to June 2026 on 9, 15 and 18 mm panels averaged 0.014–0.032 ppm, against the CARB Phase 2 limit of 0.05 ppm.
The factory shows its floor. We send real photos and video of production, and we walk you through the factory on a video call or in person. Every container is photographed and filmed before it is sealed.
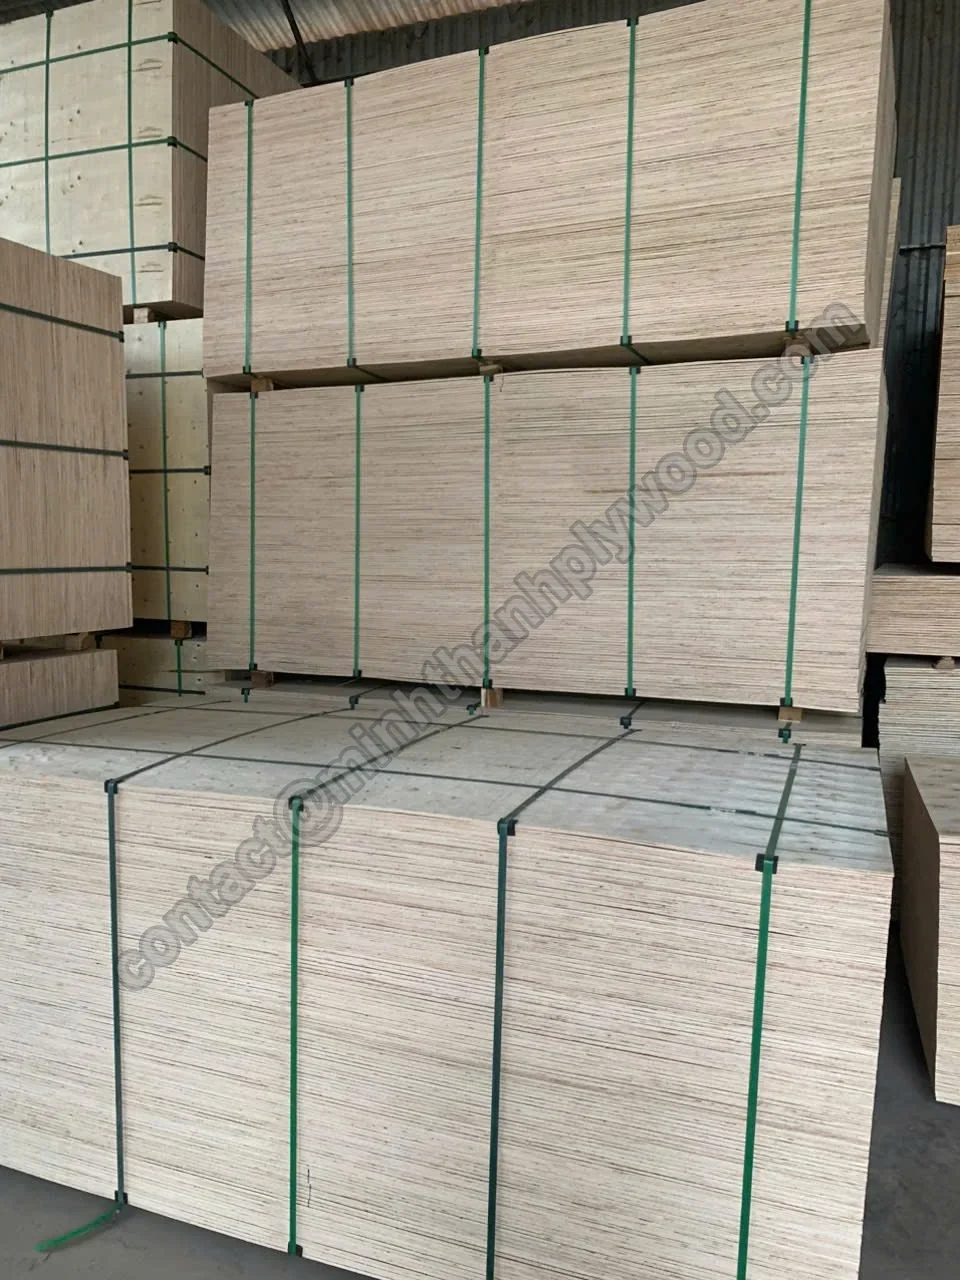
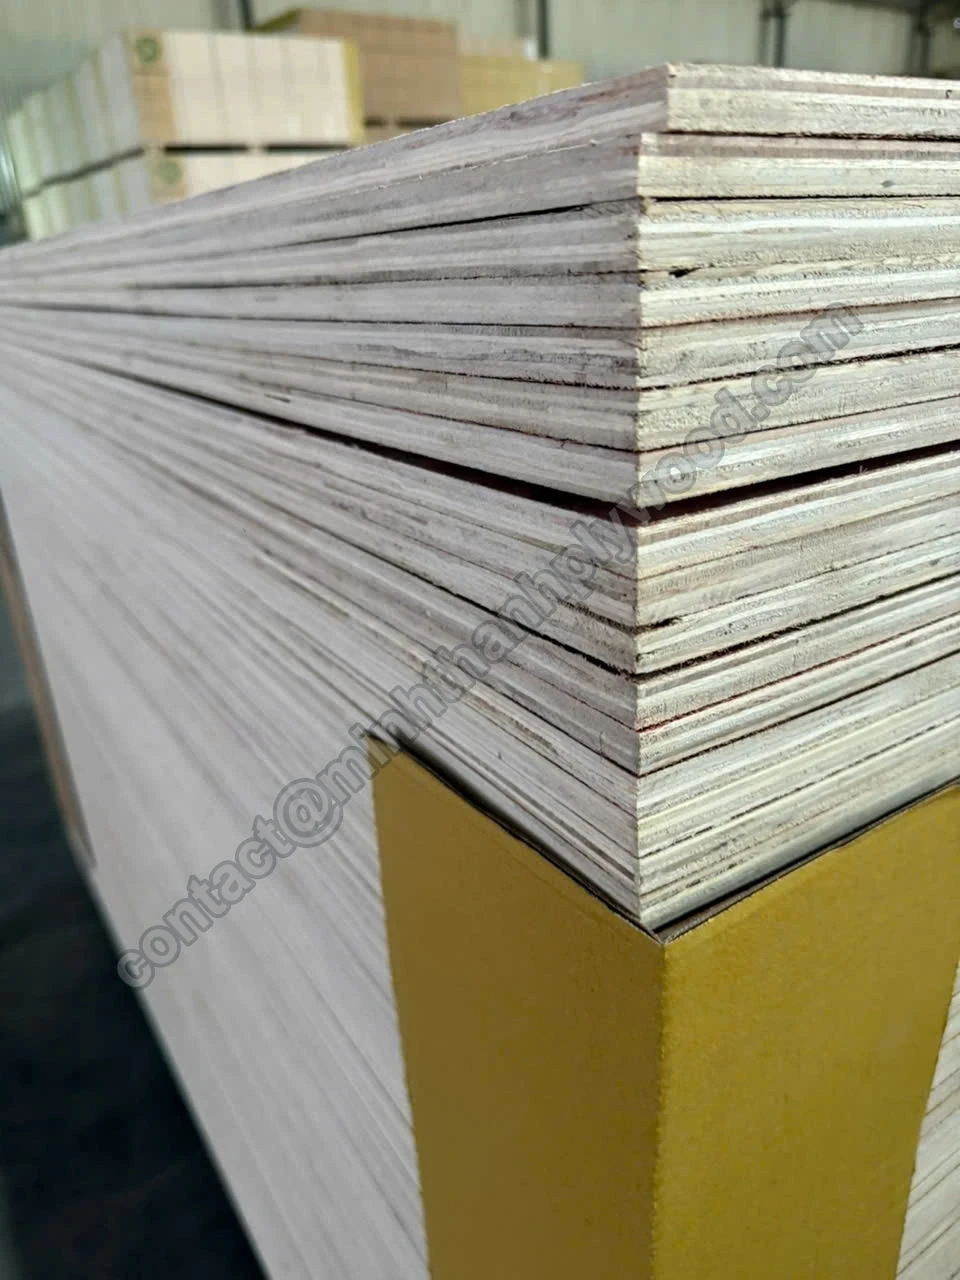
The edge tells the truth about the core. Core species, ply count and joints show on every cut edge, so ask for edge photos of your own order, not stock pictures. We build every container to the approved sample, not only the first one.
Compliance files exist before the order. For Europe we supply the EUDR compliance dossier (origin records and geolocation files), and an SGS packaging test under Regulation (EU) 2025/40: lead, cadmium, mercury and hexavalent chromium were not detected in all four packaging materials.
How to visit and audit our factory
Buyer visits and third-party inspections are part of normal business at Minh Thanh.
- Ask for the files first. Email us for the certificates, test reports and EUDR files, and check the numbers with the issuers.
- Book a video walk-through. We show the production floor, the presses, sanding and packing live, at a time that suits your office.
- Agree the date of your visit. Tell us your dates and what you want to see; we plan production so your panels are on the line.
- Inspect on site. Check veneer, lay-up, pressing, sanding and finished packs; measure panels with your own caliper.
- Keep the record. Take photos and readings, or appoint an agency such as SGS, Intertek or Bureau Veritas before loading.
| What to check | Why it matters | What we provide |
|---|---|---|
| Certificate holder and mill number | Proves which plant makes the panels | CARB P2 / TSCA Title VI, ICTT mill no. 23024; ISO 9001:2015 KAC25/0185 |
| Emission test reports | E0 means little without a test method | ASTM D6007 chamber results, every 3 months |
| Live production | Traders cannot show a floor on demand | Video-call walk-through and on-site visits |
| Edge photos of your order | Shows the real core and ply count | Edge and caliper photos in every shipment record |
| Packaging compliance | Needed for EU packaging rules | SGS PPWR test, September 2026 |
| Timber origin | Needed for EU due diligence | EUDR compliance dossier: origin records and geolocation files |
| Trade terms in writing | Avoids surprises after the deposit | MOQ, lead time, payment and Incoterms on this page |
Factory visits welcome
Visit our plywood factory, or inspect before loading.
We host buyer visits and inspections at our Vietnam plywood factory in Ha Hoa. Come before your first order to see the lines, or send your inspector before loading. If you cannot travel, the photo and video record of your container reaches you before it is sealed.
- On-site visits by appointment, Monday–Friday
- Video-call walk-through of the production floor
- Your own inspector or a third-party agency before loading
- Caliper readings, faces and edges of your panels
- Photos and video of every container before sealing
Planning a trip to northern Vietnam? Tell Lisa your dates and we arrange the visit around your schedule.
Markets
Where our plywood goes, and what each market asks for.
Europe is our strongest market, and we export across the Americas, Asia and Africa. Each market asks for different files and construction, and we prepare them as standard.
Europe
Regular shipments to European buyers, with light Styrax cores, fine faces, tight tolerance, EUDR origin files and the SGS packaging test.
Italy
Repeat orders, including cut-to-size furniture panels: one 1220 × 2440 or 1250 × 2500 mm sheet cut into 4, 6 or 8 pieces.
The Americas
Products that meet US requirements: UF glue at E0 emission and CARB P2 / TSCA Title VI certification under ICTT mill no. 23024. Imperial sizes are made to their metric equivalents.
Asia
Furniture, commercial and packing plywood, built to the density, glue and emission your market specifies.
Africa
Commercial, packing, film-faced and furniture plywood in full containers, with mixed loads by agreement.
Any market
Start from the end use. Tell us what the panel will become and we set the core, glue, face and tolerance to match.
Documents for every market: commercial invoice, packing list, B/L, certificate of origin, phytosanitary and fumigation certificates where required, and insurance on CIF shipments.
Capacity
50,000+ m³ of plywood a year: what our capacity means in containers.
Minh Thanh Plywood makes 50,000+ m³ of plywood a year, over 4,000 m³ a month. At 53–54 m³ per 40HC with a Styrax core, that is more than 75 containers a month across furniture, commercial, packing and construction panels. Every panel is built to one approved sample under the same checks and certificates, and production runs 15–45 days after deposit.
See the product rangeWhy buyers choose us
Six reasons importers choose this plywood company in Vietnam.
Importers choose Minh Thanh for six reasons, and each one is backed by proof shown on this page.
- 01
A real manufacturer
Our own production, real factory photos and videos, and certificates in our own name with their numbers.
- 02
Ha Hoa price for the grade
Local plantation cores and a skilled workforce: high-grade quality at a better price than comparable mills.
- 03
Demanding specs as routine
Stitched cores, UF glue at E0 emission, down to ±0.2 mm, sanded and polished UV-ready faces on every furniture order.
- 04
Files Europe and the US need
CARB P2 / TSCA Title VI, E0 test reports, the SGS PPWR test and EUDR geodata, ready before you order.
- 05
Flexible orders
Custom sizes, cut-to-size, 10+ faces and mixed loads by agreement from one 40HC.
- 06
Fast, direct contact
Lisa replies within hours by email or WhatsApp, and every container is photographed and filmed before sealing.
Questions buyers ask
Vietnam plywood factory FAQ.
Short answers to the questions buyers ask most about our factory.
Where is your Vietnam plywood factory?
In Ha Hoa, Phu Tho province, northern Vietnam, among the plantation hills that supply our Styrax and Eucalyptus cores. Containers are loaded at the factory and shipped FOB Hai Phong, CFR or CIF.
Are you a manufacturer or a trading company?
A manufacturer. Minh Thanh Plywood makes its own panels in Ha Hoa, holds CARB P2 / TSCA Title VI under ICTT mill no. 23024 and ISO 9001:2015 for plywood manufacturing, and shows you the production floor in person or on video.
What is your production capacity?
We make 50,000+ m³ of plywood a year: over 4,000 m³ a month, or more than 75 × 40HC containers at 53–54 m³ each. Production takes 15–45 days after deposit.
How long have you been making plywood?
Our team has over 20 years of plywood-making experience, mostly in high-grade furniture and interior panels.
Can I visit the factory?
Yes. We host buyer visits and inspections by appointment, Monday to Friday. Tell Lisa your dates and we plan production so your panels are on the line when you arrive; a live video-call walk-through is ready if you cannot travel.
Can a third-party inspector check my order?
Yes. Your own inspector or an agency such as SGS, Intertek or Bureau Veritas is welcome during production or before loading. We also send caliper readings, face and edge photos and video of every container before sealing.
Which products does the factory make?
High-grade furniture and interior plywood with Birch, Poplar, EV, Okoume, Pine and other faces, plus commercial, packing, film-faced, anti-slip and exterior plywood and LVL. Thickness is 3–40 mm in 1220 × 2440, 1250 × 2500 mm or custom sizes.
Which cores do you use?
White Styrax or Eucalyptus from local plantations for furniture panels; Acacia or Eucalyptus for film-faced and anti-slip. Product names follow the face, so birch-faced plywood is a birch face on a Vietnamese core.
Which certificates do you hold?
CARB P2 / TSCA Title VI (ICTT mill no. 23024), ISO 9001:2015 (KAC25/0185) and TCVN 11902:2017. E0 emission is tested every 3 months, and our packaging passed an SGS PPWR test in September 2026. FSC and CE are available*. *Supplied directly or through qualified partner mills.
Can you supply EUDR documents?
Yes. We supply the EUDR compliance dossier (origin records and geolocation files) with orders, for your due diligence under Regulation (EU) 2023/1115.
What is the minimum order?
One 40HC container. Most containers carry 1–2 products, and 3–6 products can be mixed by agreement.
What are your payment terms?
30% deposit and 70% against the scanned bill of lading, by T/T or irrevocable L/C at sight.
Do you send samples?
Yes, free samples. Tell us the face, core, thickness and glue you want to test.
How much plywood fits in a 40HC?
With a Styrax core, up to 18 packs and 53–54 m³ fit in one 40HC; with an Acacia core, about 47 m³. Heavier cores reach the container weight limit sooner, so we plan every load by thickness and core.
How is plywood made at your factory?
Plywood is made by peeling plantation logs into veneer, drying and grading it, gluing cross-banded layers, then cold and hot pressing and sanding to thickness. Our furniture panels are pressed twice and sanded down to ±0.2 mm, and every pack is caliper-checked before export packing.
Get a quotation
Send your specification, or book a factory visit.
Tell us the end use, face, core, glue, thickness, size and quantity. Lisa replies within hours by email or WhatsApp, Monday–Friday 08:00–17:00 Vietnam time. Free samples, and factory visits by appointment.
[email protected]